The Importance of Industrial Humidity Control: A Decision Guide for Production Managers
For most production managers, humidification is treated as a "by-product of the HVAC system" and is pushed to the bottom of the budget conversation. Yet across Türkiye's geography, indoor relative humidity (RH) falls into the 20–30% band for roughly six months between October and March; during this period production efficiency drops, product quality drifts, employee absenteeism climbs, and energy consumption silently rises. This guide explains, through three core topics — static electricity, moisture stability, and health & comfort — why industrial humidification is not an "added cost" but rather a measurable, return-bearing investment. It is designed as a decision guide that production managers can put to work directly. As NKT – Nem Kontrol Teknolojileri, we summarise here our equipment-selection and technical-service experience as Neptronic's authorised distributor in Türkiye.
Three Core Problems Caused by Low Relative Humidity
Three main headings form the economic rationale for an industrial humidification investment: static electricity (direct effect on production efficiency and product quality), moisture stability (dimensional, textural, and weight stability of hygroscopic materials), and health & comfort (employee absenteeism, IAQ complaints, and heating cost). Each of these contributes to the return on a humidification investment; the payback period is calculated from the facility-specific values of these items. The three cards below summarise the business impact of each heading at a glance.
Loss of efficiency and safety: paper sticking in print rooms, yarn breakage in textile, PCB failure in electronics, flammable-gas sparks in operating rooms. ESD risk rises dramatically below 35% RH.
Product quality: cotton, paper, wood, tobacco, leather all equilibrate with ambient air (hygroscopic regain). RH fluctuation = drift in size, texture, weight.
Employee productivity: mucosal irritation, virus susceptibility, absenteeism. RH 20→30% transition reduces absenteeism by 15%; comfort thermostat can be lowered by 1–2°C.
In the sections below we examine each heading in detail, covering sector-specific effects and the parameters production managers should weigh when making a decision. For computation, our Psychrometric Calculator tool is available.
Static Electricity and Production Efficiency
Static electricity arises from electron exchange when two surfaces rub against each other. The intensity of this phenomenon is directly affected by air humidity: humid air, owing to its water molecules, allows electron transfer to dissipate over a surface, and the electrical charge bleeds off gradually. In dry air, however, charge accumulates on the surface and discharges directly onto a metallic object or operator — this both reduces production efficiency and causes failures in sensitive electronic components (PCB, sensor, chip). The widely accepted critical threshold in industry is 35% RH; below this value, static-related complaints rise exponentially.

Sector-Specific Impact Table
The economic impact of static electricity on production varies by sector. The table below summarises typical observations widely reported in international engineering literature.
| Sector | Static-Electricity Effect | Typical Efficiency Loss |
|---|---|---|
| Printing & Press | Paper sticking, feed jams, high-speed press stoppages, ink misting | Production speed loss |
| Textile (Cotton, Synthetic) | Yarn adhesion, shuttle slip, weave-pattern defects, fiber breakage | Line downtime |
| Office & Photocopying | Photocopier jams, print scatter, static-shock complaints | Increase in service call volume |
| Computer Room & Data Center | PCB failure, tape-drive breakage, sensor noise, reset errors | ESD-related failure cost |
| Hospital Operating Room | Flammable anesthetic gas + static spark = explosion risk (critical & life-threatening) | Patient safety — zero tolerance |
| Electronics Assembly (SMT) | Chip ESD damage, sensor failure, calibration drift | Drop in lot acceptance rate |
For deeper coverage of static electricity, see our ESD (Electrostatic Discharge) and static electricity glossary entries. In sensitive electronics production environments, mapping ESD risk and setting the humidification setpoint in the 40–50% RH band is common practice.
Moisture Stability: The Silent Determinant of Product Quality
Hygroscopic (water-attracting) and fibrous materials — cotton, wool, paper, wood, tobacco, leather, gelatin, starch — equilibrate dynamically with ambient moisture. A change in ambient humidity directly changes the material's moisture content by mass: it absorbs or releases water — resulting in shifts in dimension, texture, weight, and mechanical properties. In engineering literature this phenomenon is called hygroscopic regain. When the ambient relative humidity is held at a given value, the material absorbs the corresponding equilibrium moisture percentage.
What Does the Loss Mean?
Hygroscopic regain is not an abstract engineering concept; it shows up directly as a gain/loss line item in the operations ledger. Let us make it concrete with a few practical examples:
- Tobacco: A transition from 5% RH to 50% RH means 11–16% mass gain for cigarette tobacco. The number of cigarettes that can be produced from the same quantity of tobacco varies by this margin; when production is run in low-RH conditions, the operation loses 110–160 kg of saleable product per ton of tobacco.
- Cotton (American): Moving from 10% RH to 50% RH lifts regain from 2.6% to 5.9%; this corresponds to roughly 3.3% mass gain. Moisture content is a pricing parameter in cotton trade.
- Wood (lumber): A rise from 30% to 60% RH causes a 2–3% dimensional expansion. For a furniture manufacturer this translates directly into assembly defects, sticking doors and drawers.
- Paper: Printing paper regain rises from 5% to 7% as RH moves from 30% to 50%. This shift disturbs the paper's dimensional stability — the root cause of register drift, curl, and wrinkle complaints.
- Leather: Hardens and cracks at 30% RH; becomes pliable at 70% RH. In tanning and leather garment production, the RH band should be fixed at 50–55%.
Typical Equilibrium Ranges for Türkiye Industry
The table below summarises typical design humidity ranges for the most common hygroscopic materials encountered in Turkish industry, derived from ASHRAE fundamentals. For detailed sector-specific design conditions see the ASHRAE Table 4 reference in our Humidification Load Calculation guide.
| Sector / Material | Typical RH Band | Design Temperature |
|---|---|---|
| Textile — Cotton Weaving | 60–65% | 24°C |
| Textile — Cotton Combing | 50–60% | 22°C |
| Printing — Press Room | 45% | 24°C |
| Paper Warehouse | 50% | 24°C |
| Tobacco — Cigarette Processing | 60–70% | 24°C |
| Furniture — Woodworking | 40–45% | 20°C |
| Museum, Archive, Library | 50–55% | 21°C |
| Food Storage (Dry) | 50–55% | 15–20°C |
| Leather Tanning | 50–55% | 22°C |
Hygroscopic Regain: Reference Table
The table below is the most frequently referenced hygroscopic regain dataset in industrial engineering literature (based on the ASHRAE Handbook and Carrier System Design), reorganised by NKT engineering. Percentages express moisture as a fraction of dry weight: at a given RH equilibrium, what percentage of the material's dry mass is water? This table is the fundamental reference for setting an ambient RH setpoint in product quality control. Our hygroscopic regain glossary entry defines the concept in detail.
Hygroscopic Regain of Common Industrial Materials (at % RH)
| Sector / Material | 10% | 20% | 30% | 40% | 50% | 60% | 70% | 80% | 90% |
|---|---|---|---|---|---|---|---|---|---|
| Bakery / Confectionery | |||||||||
| Cracker | 2.1 | 2.8 | 3.3 | 3.9 | 5.0 | 6.3 | 8.2 | 10.9 | 14.9 |
| Flour (White Wheat) | 2.6 | 4.1 | 5.3 | 6.5 | 8.0 | 9.9 | 12.4 | 15.4 | 19.1 |
| White Bread | 0.5 | 1.7 | 3.1 | 4.5 | 6.2 | 8.5 | 11.1 | 14.5 | 19.0 |
| Leather | |||||||||
| Sole Oak Tanned | 5.0 | 8.5 | 11.2 | 13.6 | 16.0 | 18.3 | 20.6 | 24.0 | 29.2 |
| Printing / Paper | |||||||||
| Newsprint (24% Ash) | 2.1 | 3.2 | 4.2 | 5.3 | 6.2 | 7.2 | 8.3 | 9.9 | 11.9 |
| White Bond Rag (1% Ash) | 2.4 | 3.7 | 4.7 | 5.5 | 6.5 | 7.5 | 8.8 | 10.8 | 13.2 |
| Writing Paper (3% Ash) | 3.2 | 4.2 | 5.0 | 5.9 | 6.8 | 8.2 | 9.9 | 11.8 | 14.2 |
| Textile | |||||||||
| Cotton — Absorbent | 4.8 | 9.0 | 12.5 | 15.7 | 18.5 | 20.8 | 22.8 | 24.3 | 25.8 |
| Cotton — American | 2.6 | 3.7 | 4.4 | 5.2 | 5.9 | 6.8 | 8.1 | 10.0 | 14.3 |
| Cotton — Sea Isle | 2.4 | 3.5 | 4.3 | 5.1 | 5.8 | 6.8 | 8.2 | 10.3 | 14.1 |
| Abaca (Manila) / Sisal | 4.9 | 7.8 | 9.9 | 11.5 | 13.1 | 14.9 | 17.2 | 20.2 | 24.1 |
| Jute | 3.1 | 5.4 | 7.7 | 9.7 | 11.4 | 13.1 | 15.2 | 17.8 | 20.2 |
| Linen — Dry Spun | 1.9 | 2.9 | 3.6 | 4.3 | 5.1 | 6.1 | 7.0 | 8.4 | 10.2 |
| Rayon — Acetate / Filament | 0.8 | 1.1 | 1.4 | 2.3 | 2.8 | 3.4 | 4.1 | 5.3 | 7.3 |
| Rayon — Cuprammonium | 1.8 | 3.3 | 4.8 | 6.7 | 8.8 | 10.9 | 12.9 | 15.8 | 19.5 |
| Rayon — Viscose | 2.8 | 4.0 | 5.7 | 6.9 | 8.1 | 10.0 | 11.9 | 14.3 | 18.8 |
| Silk — Raw Chevennes-Skein | 3.2 | 5.5 | 6.9 | 8.0 | 8.9 | 10.2 | 11.9 | 14.3 | 18.3 |
| Wool — Australian / Merino-Skein | 4.7 | 7.0 | 8.9 | 10.8 | 12.8 | 14.9 | 17.2 | 19.9 | 23.4 |
| Tobacco | |||||||||
| Cigarette | 5.4 | 8.6 | 11.5 | 14.3 | 16.8 | 19.8 | 23.5 | 28.5 | 34.5 |
| Wood | |||||||||
| Lumber — Average | 2.3 | 4.7 | 6.8 | 9.1 | 11.4 | 13.7 | 16.5 | 19.9 | 23.7 |
| Glue — Hide | 3.4 | 4.8 | 6.6 | 8.3 | 10.5 | 12.5 | 14.2 | 16.2 | 19.0 |
| Miscellaneous | |||||||||
| Activated Carbon — Steam | 7.1 | 14.3 | 22.8 | 26.2 | 28.3 | 29.2 | 30.0 | 31.1 | 32.7 |
| Gelatin | 2.8 | 4.9 | 6.6 | 8.1 | 9.5 | 11.4 | 13.2 | 15.2 | 17.8 |
| Silica Gel | 5.7 | 9.8 | 12.7 | 15.2 | 17.2 | 18.8 | 20.2 | 21.5 | 22.2 |
| Soap | 1.9 | 3.8 | 5.7 | 7.6 | 10.0 | 12.9 | 16.1 | 19.8 | 23.8 |
| Starch | 2.2 | 3.8 | 5.2 | 6.4 | 7.4 | 8.3 | 9.2 | 10.6 | 12.7 |
Note: Moisture percentage based on dry weight, ambient temperature 22°C. Source: Derived from ASHRAE Handbook and Carrier System Design datasets by NKT.
When working with the hygroscopic regain table, do not neglect the band width (±% RH). Targeting 50% ± 2% RH demands very different equipment accuracy and control strategy than 50% ± 5% RH. For applications requiring tight control, the Neptronic SKE4 / SKS4 family (±1% RH) is preferred; for comfort applications, Neptronic SKH atomization (±3–5% RH) is selected.
Health & Comfort: The Non-Obvious Dimension of Employee Productivity
When production efficiency is discussed, machines come to mind first; yet one of the most critical factors shaping production rate in the field is employee health and comfort. In winter, the heating system pushes indoor relative humidity down to the 20–30% range. Such dry air triggers a series of adverse effects in the human body: drying of the upper-respiratory mucosa, eye irritation, skin cracking, static-shock complaints, headaches, and general fatigue. More critically, dry air extends the suspension time of viruses and bacteria; it lowers mucosal defence capacity. The result: a rise in sickness frequency, an increase in absenteeism, and a silent loss of production capacity.

Absenteeism and Cost
The classic study by Dr. George Green of the University of Saskatchewan showed that raising relative humidity from 20% to 30% reduced employee absenteeism by approximately 15% in an office environment. Such a reduction in absenteeism can be treated as a separate line item in the return calculation.
Indoor Air Quality (IAQ)
A significant share of Indoor Air Quality (IAQ) complaints is comfort-driven: air feeling too dry, too humid, too warm, or too cold. The majority can be resolved with correct humidity control. ASHRAE 55 sets no lower relative humidity limit for thermal comfort and gives its upper limit as a humidity ratio of 0.012 kg/kg (≈ 12 g/kg). The 30–50% RH band is the optimal range from comfort, microbiology, and electrostatic standpoints alike:
- Bacteria: Most bacteria show minimum proliferation in the 30–60% RH band.
- Virus: Influenza and respiratory viruses stay viable far longer in dry air (below 20%); inactivation accelerates in the 40–60% band.
- Fungi / Mould: Growth rises dramatically above 60% RH; keeping RH below 60% keeps mould risk under control.
- Dust mites: Population grows above 50% RH; below 50% it remains controlled.
- Respiratory tract issues: Asthma, allergy, and COPD complaints are minimised in the 30–50% band.
Comfort Thermostat: Silent Energy Saving
A frequently overlooked fact: humid air feels warmer. At the same measured temperature, the humid environment is perceived 1–2°C warmer than the dry one. This means that, once humidification is in service, the heating thermostat can be lowered by 1–2°C. This strategy can reduce heating costs by 5–10%. The humidification investment therefore contributes not only to comfort but also positively to the energy budget.
Sector-Specific Impacts and Economic Costs
The economic cost of low relative humidity is realised through a different mechanism in each sector. The table below summarises typical areas of impact reported in international industry sources; actual values vary by facility and should be verified with the facility's own data.
| Sector | Mechanism of Low RH | Measurable Cost |
|---|---|---|
| Printing | Active paper waste (curl + register + static), press re-runs, ink misting | Higher paper and print waste |
| Textile (Yarn / Weaving) | Yarn breakage, static-shock downtime, shuttle slip, fiber dusting | Production loss from line downtime |
| Data Center / Computer Room | ESD product failure, sensor noise, reset errors, tape-drive damage | ESD-related failure cost |
| Hospital (HAI) | Airborne infection transfer (mucosal defence drop, virus viability) | Higher infection risk (low RH) |
| Museum & Archive | Wood cracking, paper disintegration, paint flaking, leather drying | High future restoration cost |
| Food Storage (Fruit-Vegetable) | Evaporation-driven weight loss, surface shrivelling, sales loss | Weight loss |
| Furniture / Wood | Lumber dimensional drift, assembly defects, door/drawer sticking, returns | Higher assembly return rate |
| Tobacco Processing | Dry-tobacco weight loss, loss of elasticity, cigarette-machine speed loss | 11–16% mass loss (RH 50%→5%) |
| Pharmaceutical | Tablet cracking, coating failure, capsule electrostatic charge | Drop in lot acceptance rate |
Investment and Return Calculation
An industrial humidification investment fits a classical CAPEX + OPEX model. The items below show the headings to consider in a mid-size application; amounts vary by capacity, technology and facility, so they must be calculated for each project.
Cost Items (Typical Mid-Size, 5–50 kg/hr)
- Equipment CAPEX: Varies by capacity and technology (resistive, gas-fired, atomization).
- Installation + Mechanical: Steam distribution piping, water treatment, electrical installation and control wiring; within the installer's scope.
- Water & Energy OPEX:
- Resistive steam (SKE4): roughly 0.75 kWh/kg of steam, accurate modulation, independent of water quality.
- Adiabatic atomization (SKH): electricity use is limited to pump power; because the heat of evaporation is taken from the room air, it provides cooling when cooling is needed and adds to the heating load in the heating season.
- Maintenance: Periodic maintenance depending on technology and water quality (filter, water-level sensor check, etc.).
For a detailed OPEX comparison and 10-year TCO (Total Cost of Ownership), the TCO table in our Electrode vs. Resistive Comparison guide is available.
Return Items (Typical Mid-Size Print Room)
- Waste Reduction: Paper + print + ink.
- Employee Productivity: Reduced absenteeism + fewer static-shock complaints.
- Comfort Energy Savings: Heating thermostat lowered by 1–2°C.
- Maintenance / Service Call Reduction: Static-related press machine jams.
ROI (%) = (Annual Savings − Annual OPEX) / Total CAPEX × 100
// Values are entered from the facility's own waste, energy and investment data.
Payback varies by facility and should be calculated from the facility's own waste, energy and production data. In applications requiring a tight RH band (pharma, hospital, museum), humidification is usually not an investment choice but a requirement of the process and design specification.
Which Equipment Type Suits Your Application?
Correct equipment selection depends on application type, capacity, water quality, hygienic requirements, control accuracy, and energy-source preference. NKT – Nem Kontrol Teknolojileri's equipment-selection decision tree is summarised below:
- Hygiene-critical (hospital, pharma, food): Neptronic SKE4 + clean steam with DI/RO water or SKS4 (steam-to-steam heat exchanger). Mineral-free, odourless, sterile steam.
- High capacity, natural gas preference: Neptronic SKG4 (gas-fired steam). 50–400 kg/hr modular capacity, outdoor installation option.
- Low energy + adiabatic cooling effect, textile/print: Neptronic SKH (high-pressure atomization, RO water). 70 bar, <20 μm droplets; 20, 50 and 100 kg/hr models.
- Comfort / standard industrial: Neptronic SKE4 (resistive steam). DI / RO / hard mains water compatible, ±1% RH accuracy.
Recommended Solution 1: Neptronic SKE4 (Resistive Steam)
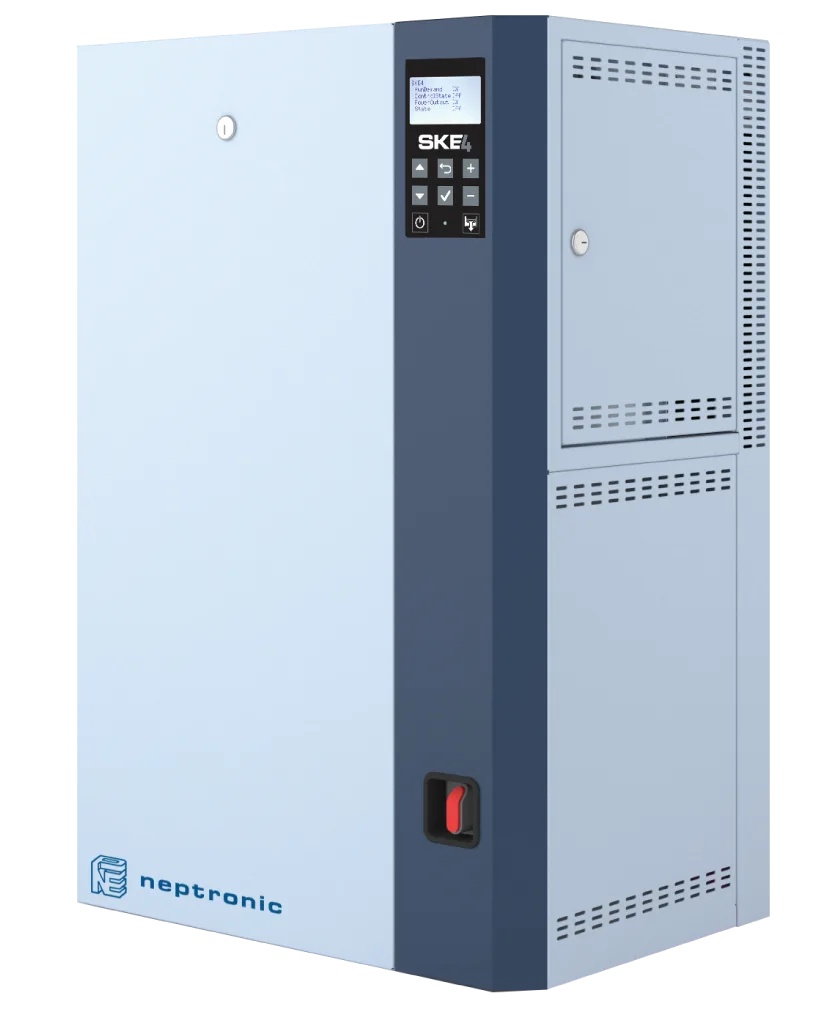
For most comfort and tight-RH applications, our first choice is the SKE4 family. It produces mineral-free, odourless, sterile steam; the long-life stainless-steel steam tank (no cylinder replacement needed), ±1% RH accuracy, and BACnet/Modbus BMS integration cover a wide application set. Its 5–120 kg/hr (50 Hz) capacity range spans from small offices to large industrial facilities.
Recommended Solution 2: Neptronic SKH (High-Pressure Atomization)
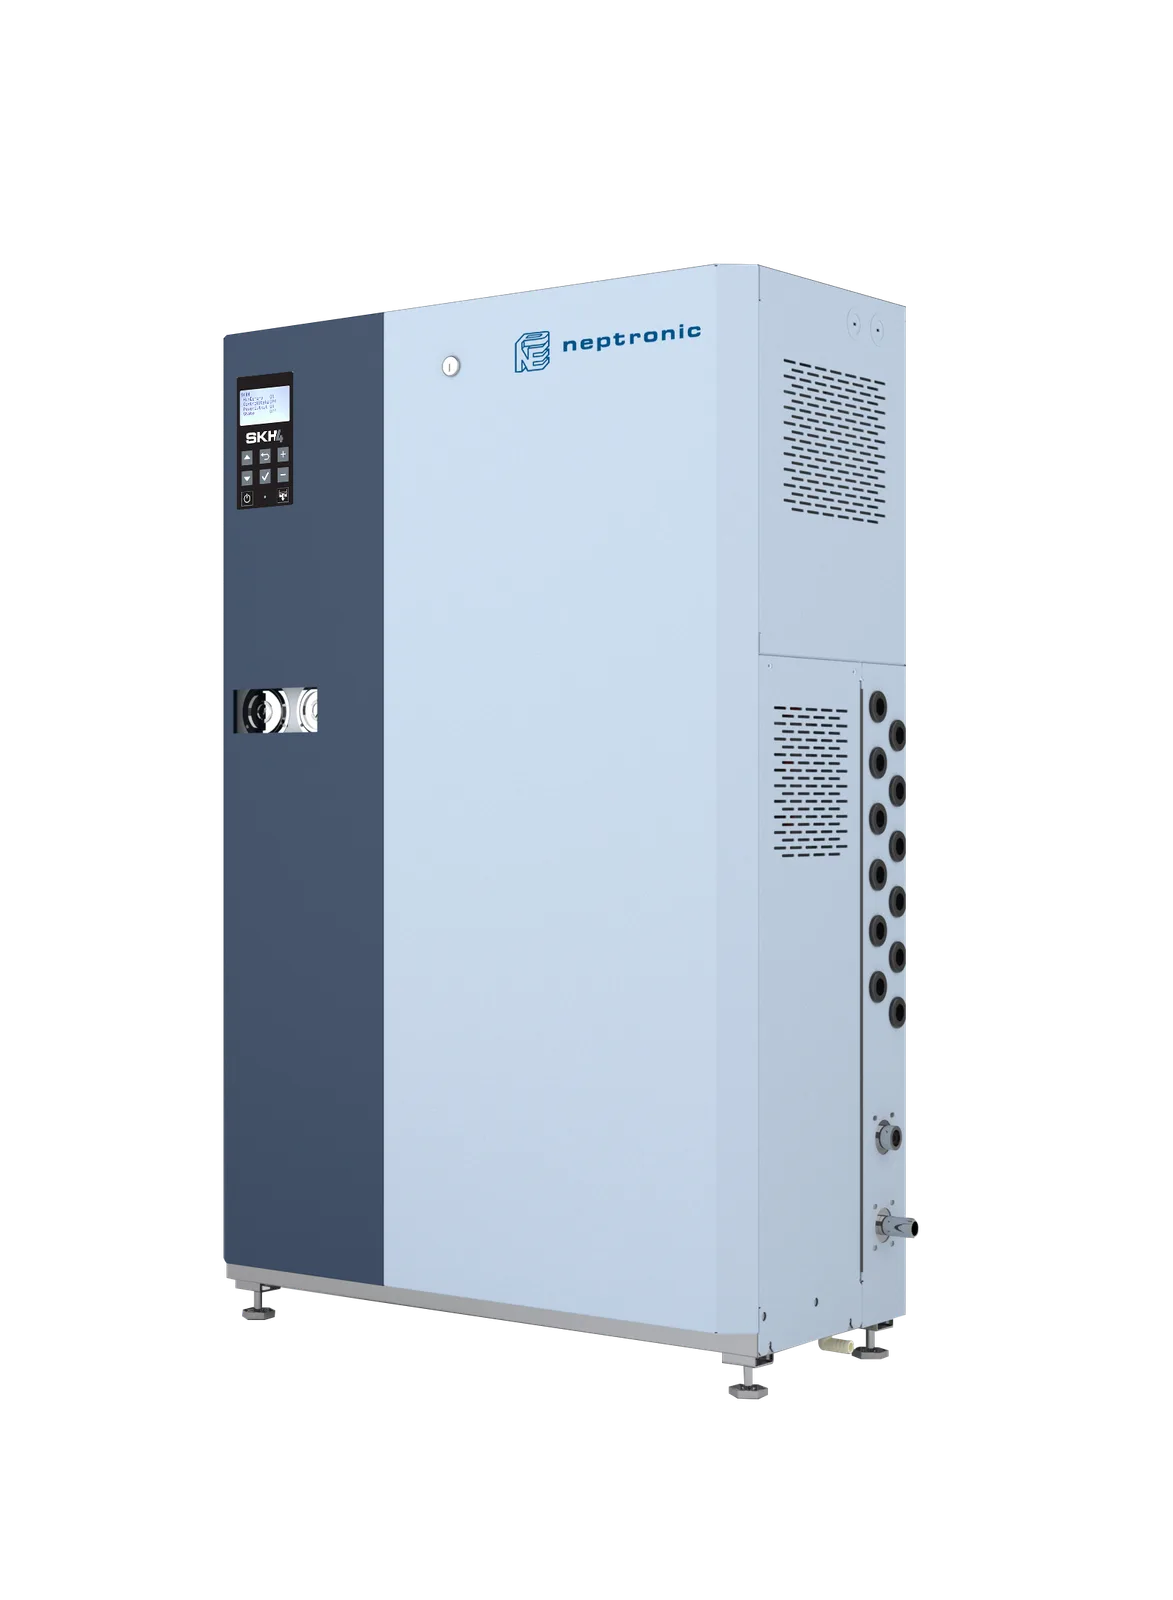
Where high airflow applications — textile, print, woodworking, greenhouse, wine cellar — meet a hard energy-budget constraint, the SKH family stands out. Adiabatic evaporation draws the latent heat from the room air and cools it. Operating at 70 bar with <20 μm droplets, the family comprises 20, 50 and 100 kg/hr models; electricity use is limited to pump power. It offers silver-ion antibacterial technology and compliance with VDI 6022 hygiene requirements.
Decision Making: Where to Start?
Approaching the industrial humidification investment decision as a four-step process delivers both technical correctness and economic transparency. This sequence is a roadmap your facility team can follow on its own, before the equipment-selection discussion.
Step 1: Measure Current RH
Through the winter season, record temperature and relative humidity once per shift (morning / mid-day / night). 3–7 days of data are sufficient. These records reveal the real profile of your current indoor conditions. An entry-level RH/temperature logger is adequate. When measuring, keep the device away from ventilation outlets, exterior doors, and heat sources.
Step 2: Define Sector-Target RH
From the design conditions table in Section 3, or for finer-grained sector records the ASHRAE Table 4 adaptation in our Humidification Load Calculation guide, identify the target RH band suited to your sector. It is important to define the band width (±% RH) together with the single setpoint, rather than the setpoint alone. The gap between target RH and your measurement is the rough indicator of your humidification load.
Step 3: Load Calculation
Hourly humidification load (kg/hr) is computed from facility volume, air-change rate, and outdoor air conditions. At this step you can use our Psychrometric Calculator tool. If you would rather not work through the math, our NKT Pro mobile app performs the entire calculation automatically from your site data; it embeds ASHRAE Climatic Design Conditions and TS 825 datasets.
Step 4: Support in Equipment Selection
With the data from the first three steps (current measurements, target RH and load calculation) you can contact us for equipment selection; we support you in identifying the right technology and model. Where additional site measurements such as a building pressure test are needed, they are carried out by the facility's mechanical designer or a measurement firm.
NKT – Nem Kontrol Teknolojileri
As NKT – Nem Kontrol Teknolojileri, we are the authorised Turkish distributor of Neptronic humidifiers; we provide equipment supply, technical support in equipment selection, technical service and spare parts. Engineering design, installation and commissioning are within the scope of the facility's design engineer and installer.
Scope of Service
- Selection support: Help in identifying the right technology and model from the Neptronic SKE4, SKS4, SKG4 and SKH families based on the facility's measurements and load calculation.
- Equipment supply: Neptronic humidifiers and steam distribution equipment.
- Technical service and spare parts: For the units we supply.
Rapid Calculation and Decision Tools
NKT's web-based free engineering tools allow production managers to perform preliminary analysis on their own:
- Psychrometric Calculator — From temperature + RH inputs, computes dew point, absolute humidity, enthalpy, and wet-bulb.
- Air Mixing Calculator — For mixed-air system design, computes the return-air + fresh-air mixing condition.
- NKT Pro mobile app — Free on iOS and Android; site equipment selection, load calculation, customer PDF report generation; works offline.
Closing
Industrial relative-humidity control must occupy a place on a production manager's agenda not as a "by-product" but as a measurable, return-bearing strategic investment. Static-electricity-driven efficiency loss, hygroscopic material stability, and employee health & comfort form three independent economic rationales; the payback period is calculated from the facility-specific values of these items. For a facility-specific preliminary analysis you can start with the NKT Pro mobile app; for support in equipment selection you can contact us.
For more information, visit our NKT Akademi homepage for the rest of our guides on psychrometrics, humidity control engineering, and sector-specific applications.