Kaşar (a Turkish pasta-filata cheese similar to kashkaval) is a semi-hard yellow cheese and one of Türkiye's most technologically demanding dairy products. Its characteristic elastic texture, balanced salt-acid profile and long shelf life depend directly on tightly controlled drying and maturation processes. During this phase, precise relative-humidity management determines both product quality and compliance with the Turkish Food Codex moisture-content limits. Poor humidity control means more than yield loss, it opens the door to mould and to microbiological risks such as Listeria monocytogenes.
This in-depth technical guide approaches kaşar cheese drying and maturation humidity control from an engineering perspective. Starting with milk processing, it covers scalding (haşlama), brining, surface drying, maturation room design, condensing vs silica gel rotor dehumidifier selection, mould prevention strategies, pathogen risk management (e.g. Listeria) and a moisture-load calculation for an example 20 ton/month plant, step by step. As NKT – Nem Kontrol Teknolojileri, our aim is to provide dairy industry engineers and plant managers with actionable, measurable and sustainable reference solutions.
Kaşar Production Process and Humidity-Critical Steps
Kaşar belongs to the pasta filata family of semi-hard yellow cheeses. Historically developed in the Thrace, Kars and Kayseri-Pınarbaşı regions of Türkiye, today it is manufactured at industrial scale under modern hygienic protocols. The Turkish Food Codex Cheese Communiqué (No. 2015/6) defines kaşar as a pasta-filata cheese that may be marketed fresh or ripened. The term "eski" (aged) may be used only for kaşar ripened for at least 120 days. The longer the ripening, the more important correct room-climate management becomes.
The communiqué sets no general minimum ripening time for kaşar; the product must meet its compositional criteria, and ripened cheese must state the ripening time on its label. This framework is the fundamental constraint of maturation room design.
General Production-Flow Schema
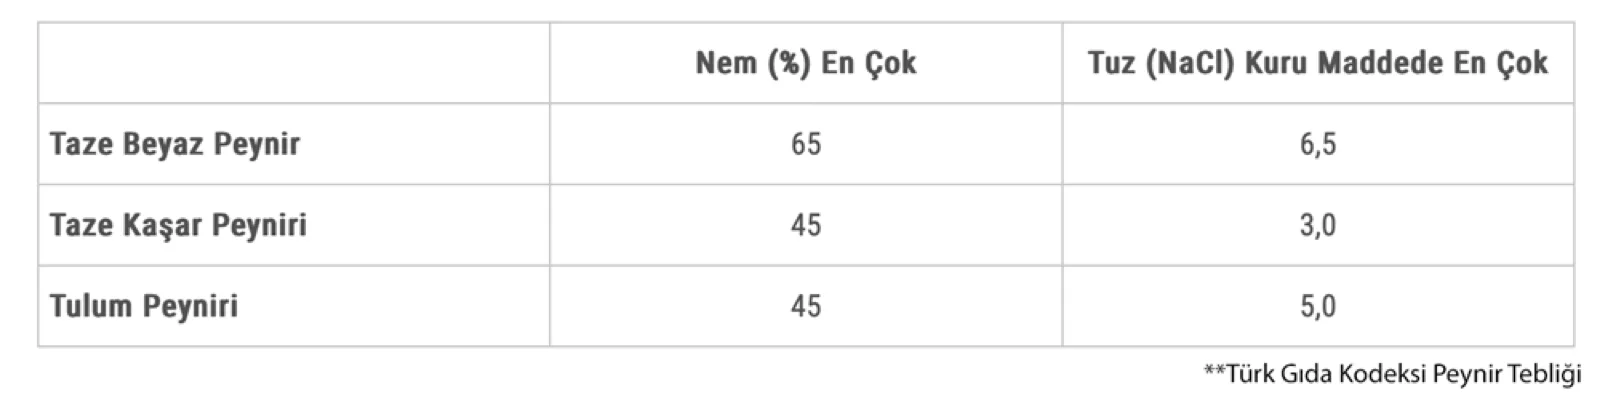
The full kaşar process flow makes it clear at which step humidity control becomes critical:
Raw milk is first pasteurized via HTST (72°C, 15 s) or LTLT (63°C, 30 min). After cooling to 30–32°C, the milk is inoculated with mesophilic Lactococcus lactis starter culture. The starter converts lactose to lactic acid; when pH reaches 6.3–6.4, rennet is added. The curd sets within 35–45 minutes and is then cut. The curd pieces undergo syneresis, expelling whey, while acidity continues to develop.
The step that truly separates kaşar from other cheeses is scalding (pasta filata). Once the curd's pH falls to about 5.1–5.3, the pieces are immersed in 70–75°C salted water and kneaded. During this stage casein protein fibres realign and the characteristic fibrous, elastic kaşar texture emerges. The kneaded mass is pressed into moulds and set with cold water. Depending on the plant's method, the shaped blocks are then salted in brine or by dry salting; the salting area must be kept cool. Salt supports flavour development while also building the initial surface barrier.
Drying Phase and Surface Rind Formation
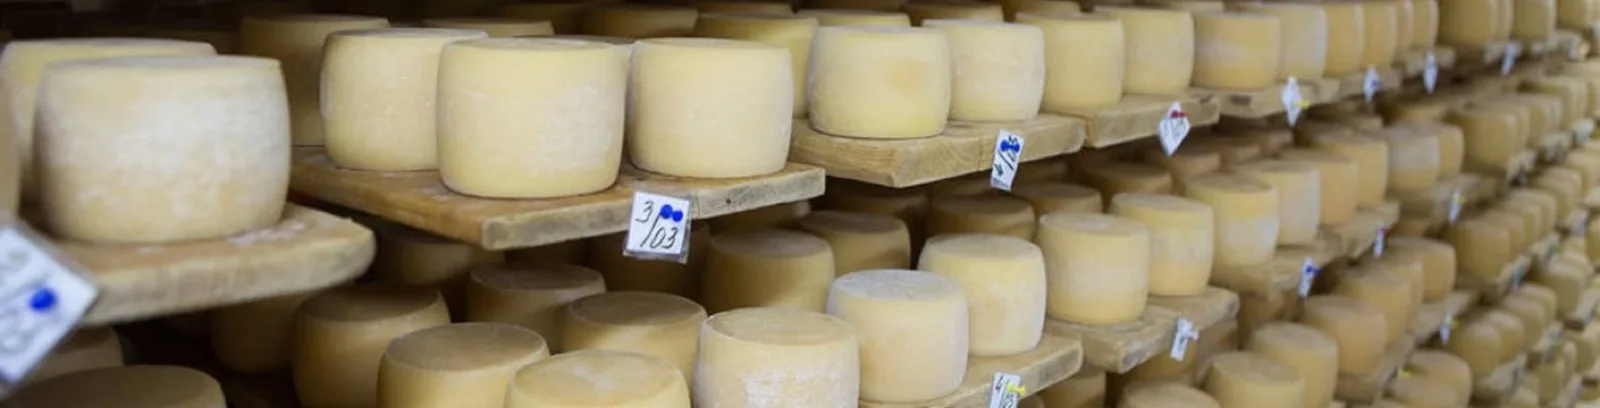
Kaşar blocks leaving the brine bath are loaded onto stainless steel (AISI 304) hygienic trolleys and transferred to the drying room. In some plants this is integrated with the maturation room; in others, a dedicated drying room precedes maturation. The fundamental goal of surface drying is to rapidly reduce water activity and initiate a healthy rind.
The Engineering Significance of the Surface Rind
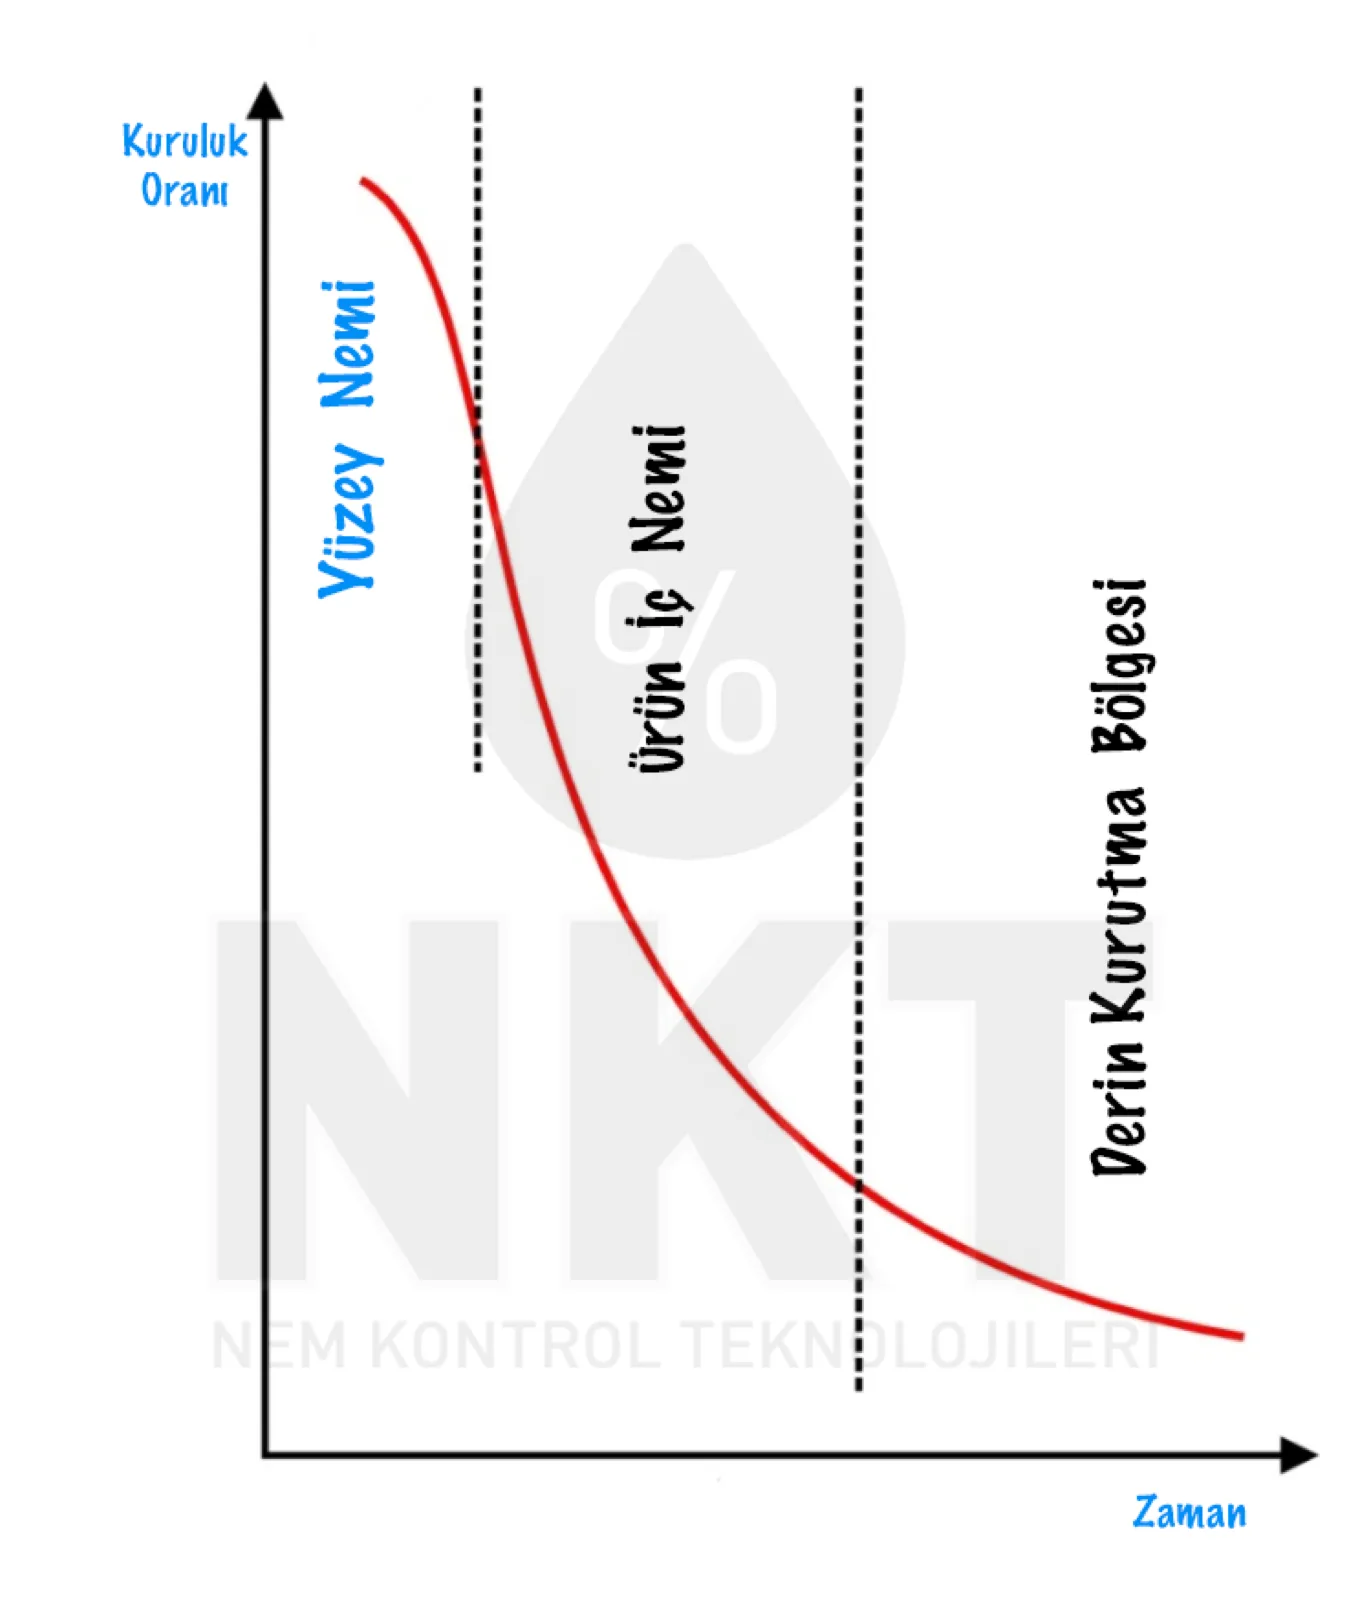
The rind acts as the cheese's "own packaging", a thin surface layer whose quality governs several functions:
- Water-vapour barrier: Releases internal moisture at a slow, controlled rate; this balances weight loss.
- Microbiological shield: As the surface dries, water activity (aw) drops; the habitat for pathogens such as Listeria and spoilage bacteria such as Pseudomonas shrinks.
- Thermal homogeneity: A dense rind buffers the internal temperature against external fluctuation.
- Flavour compartment: Keeps the volatile flavour compounds (short-chain fatty acids, esters) produced during maturation contained within the interior matrix.
Target Parameters During the Drying Phase
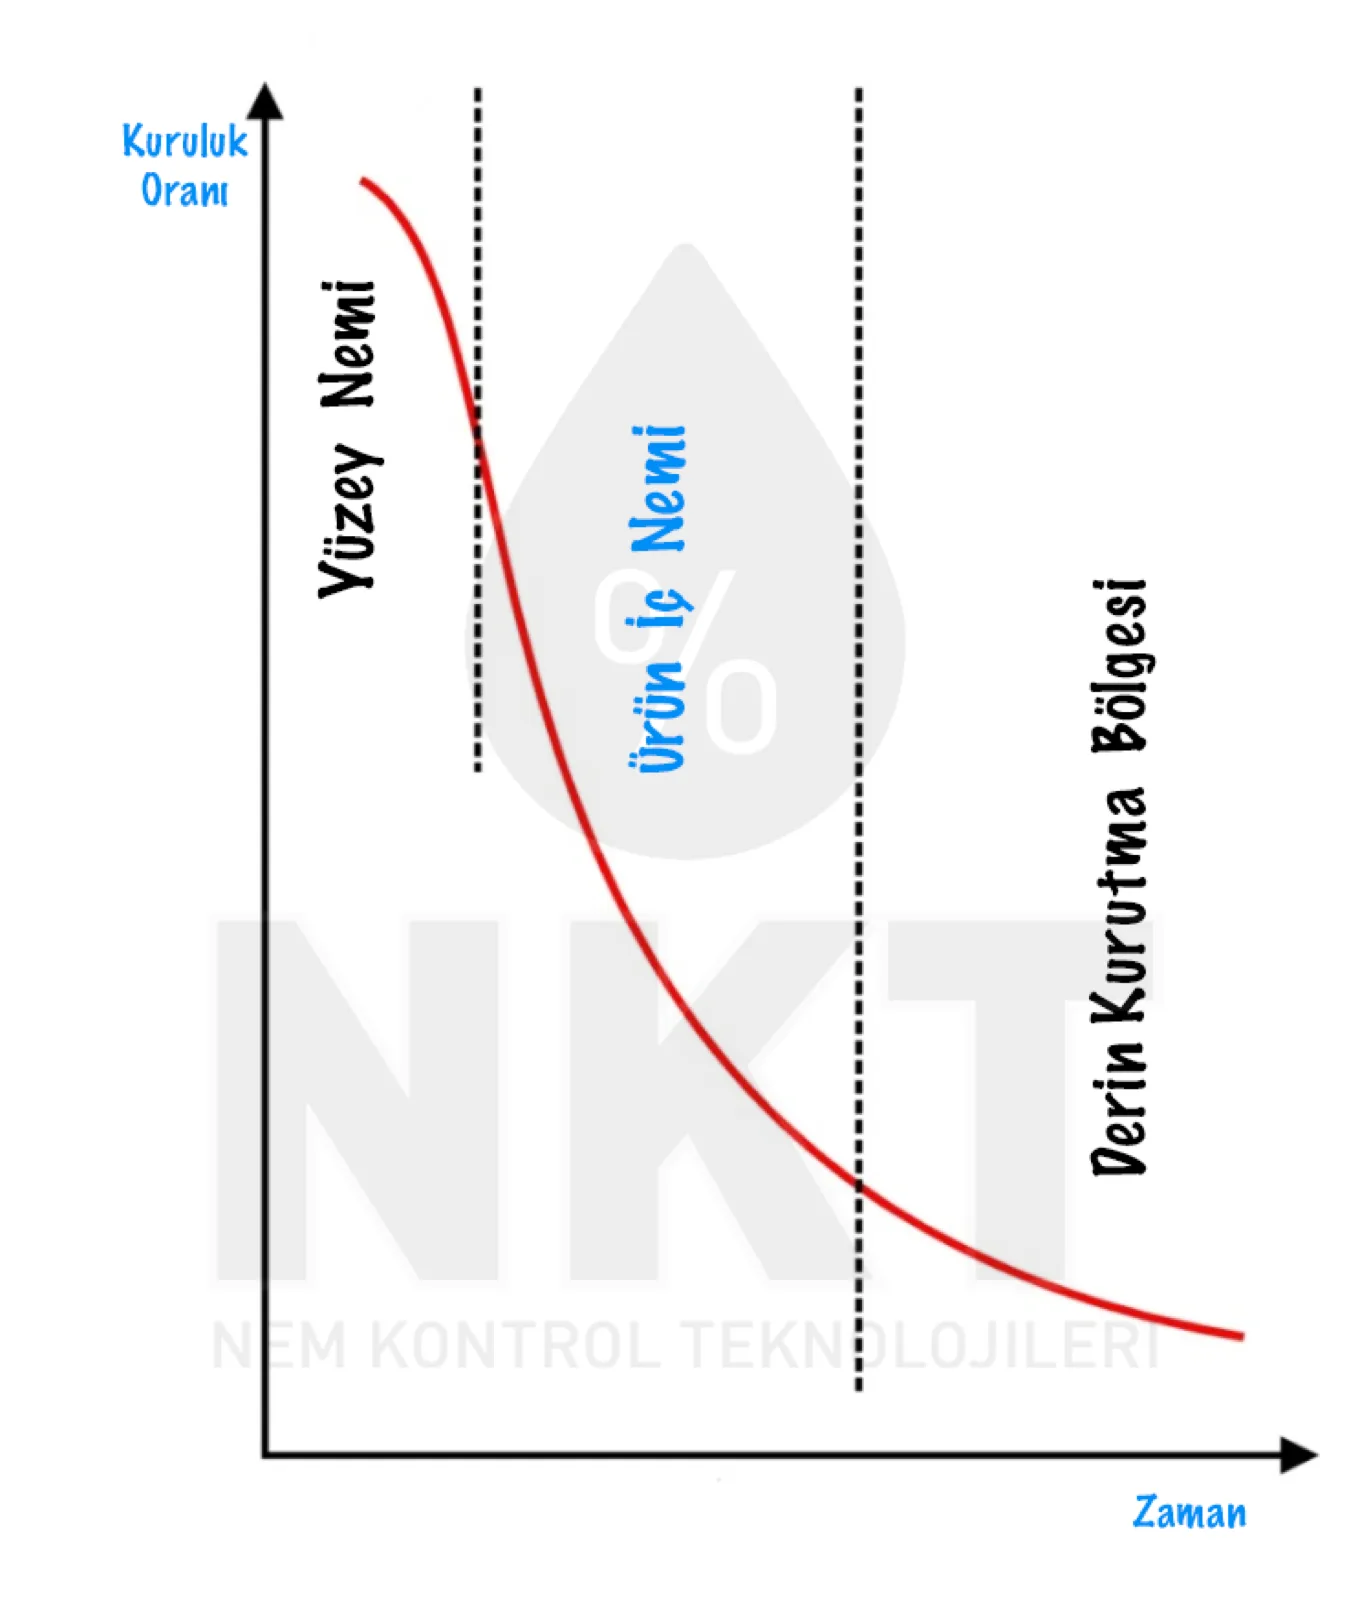
Based on kaşar practice in the literature and typical plant recipes, the following ranges can be used as starting values for surface drying (rind formation); the exact values are set by the product recipe:
| Parameter | Target Range | Tolerance Note |
|---|---|---|
| Temperature | 12–16°C | ±1°C band |
| Relative Humidity | 80–85% RH | Avoid long periods below the band (rind-cracking risk); dew point ≈ +8.7…+13.5°C |
| Air Velocity (shelf level) | 0.2–0.4 m/s | No high-velocity air directly on the rind |
| Circulation Airflow | Set by fan speed (VFD) | Chosen for shelf-level air velocity; no dead zones |
| Fresh Air | Minimum required | For CO2/odour control and slight positive pressure |
| Duration | ≈ 3–7 days | Depends on block size and recipe |
Maturation Physiology: Enzymatic and Microbial Processes
Maturation is the phase that gives kaşar its real technological identity. Biologically, three core mechanisms run in parallel: glycolysis, proteolysis and lipolysis. The rate of each is governed directly by ambient temperature and indirectly by water activity (aw), and water activity itself depends on the balance between the cheese's internal moisture and external relative humidity.
Proteolysis: The Architect of Texture and Flavour
The dominant protein in cheese, casein, is degraded during maturation by several enzyme systems. Residual chymosin from rennet cleaves casein into large peptides (e.g. β-CN f1–192). Proteases from the starter and secondary cultures then progressively break these down into smaller peptides and finally into free amino acids. Proteolysis is what produces kaşar's distinctive sliceable, elastic texture that stretches when melted.
Lipolysis and the Aroma Complex
Milk triacylglycerols are partially hydrolyzed by lipoprotein lipase and microbial lipases, releasing free fatty acids. Oxidation, esterification and subsequent reactions of these acids generate the characteristic volatile aroma profile of kaşar, notably butyric acid, caproic acid and ethyl esters. Excessive humidity and temperature accelerate lipolysis uncontrollably, producing rancid off-notes.
Glycolysis and pH Trend
During maturation, part of the lactic acid produced by the starter culture can be converted to compounds such as acetate and CO2. pH typically rises slightly from a 5.1–5.3 band to 5.3–5.5 over the first 30 days. This pH range favours mould growth, which is why keeping relative humidity below the upper limit of the maturation band (90%) and avoiding stagnant air are critical for microbiological safety.
Target Humidity and Temperature Ranges
Before packaging, the kaşar climate falls into two main phases: surface drying for rind formation and maturation for inner ripening. The ranges below are typical literature values; the exact values are set by the product recipe. In industrial production kaşar is often vacuum-packed after a short surface-drying phase and kept cold in its packaging, while rinded ripening is the traditional method.
| Phase | Duration | Temperature | Relative Humidity | Dew Point | Goal |
|---|---|---|---|---|---|
| Surface Drying (rind formation) | ≈ 3–7 days | 12–16°C | 80–85% | ≈ +8.7…+13.5°C | Removing surface water, rind formation |
| Maturation (rinded) | Per recipe; ≥ 120 days for "eski" | 10–14°C | 85–90% | ≈ +7.6…+12.4°C | Proteolysis, lipolysis; flavour and texture development |
| Cold Storage (vacuum-packed) | Until consumption | ≈ 4–7°C | Not decisive for packed product | — | Stable storage |
A key insight from this table is that temperature alone is not enough. Two different RH values at the same temperature produce two different equilibrium water activities, and therefore very different maturation behaviour. Modern dairy plants place RH sensors not at a single point, but at at least three locations: room inlet, room outlet and mid-room shelf height.
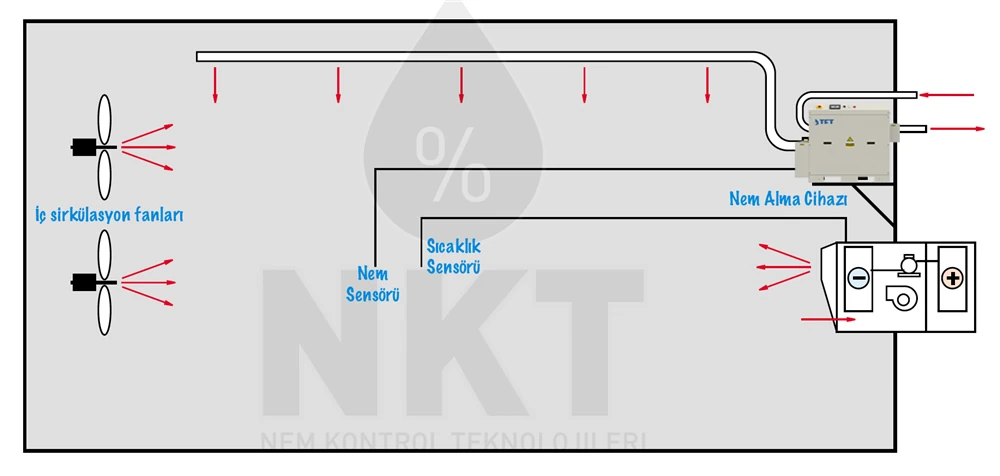
Maturation Room Design + Figure 1: Kaşar Maturation Room Cross-Section Diagram
A kaşar maturation room must be treated as an HVAC micro-climate system. The design approach holistically balances product load, cooling load, moisture load, hygienic-design criteria and energy efficiency. In this article's 20 ton/month example, each room is sized at roughly 12 m × 8 m × 4 m (LxWxH), giving a net volume of about 384 m³.
Structural Design Principles
- Sandwich panel walls/ceiling: 100–120 mm PUR/PIR polyurethane core, food-grade stainless or white-painted galvanised steel facing; thermal transmittance (U) ≤ 0.25 W/m²K.
- Floor: Epoxy-coated concrete; 1–2% slope; central drain; coved wall-floor radius for hygienic cleanability.
- Doors: Automatic sliding or hygienic swing-cushioned door; air-curtain mandatory; airlock with double doors standard on larger plants.
- Lighting: IP65 LED panels; 200–300 lux; spectra chosen for low photo-oxidation risk.
- Drainage: Independent wash-down drain lines; back-flow prevention on floor gulleys as part of hygienic design.
Air Circulation and Distribution
Success in a maturation room is directly tied to homogeneous air distribution. The target is to hold every shelf position within ±3% RH and ±1°C of the set-point. This requires:
- Slow, balanced overhead supply through textile (fabric) diffusers or perforated metal diffusers
- Floor-level return (0.3–0.5 m above the floor); moist and CO2-laden air descends
- Enough clearance between racks for air to reach every product surface
- VFD-driven circulation fans; airflow modulated to deliver 0.2–0.4 m/s at shelf level
- Fresh air kept to the minimum required; at least F7 filtration, F9 where the risk assessment calls for it
The following cross-section diagram shows the airflow architecture of a typical 12 m × 8 m × 4 m kaşar maturation room. The diagram identifies the dehumidifier, cooling coil, cheese wheels/blocks, rack layout and the direction of supply and return airflows.
Condensing vs Silica Gel Rotor Dehumidifier Comparison (Cheese Context)
The key to technology selection is the room's dew point and temperature. In the surface-drying room the dew point is about +8.7°C at 12°C / 80% RH and about +13.5°C at 16°C / 85% RH. In the maturation room it is about +7.6°C at 10°C / 85% RH and about +12.4°C at 14°C / 90% RH. These values sit right at the boundary between the two technologies.
| Room Condition | Assessment |
|---|---|
| Dew point +10°C or higher, room 15°C or warmer | Condensing units operate in their efficient zone |
| Dew point +5…+10°C, or room continuously below 15°C | Condensing units work, but capacity and COP drop; size from the low-temperature capacity curve and compare energy with a silica gel rotor or hybrid system |
| Dew point below +5°C | Silica gel rotor; in a condensing unit the evaporator ices up and defrost typically cuts capacity by 30–50% |
Condensing (Mechanical / Compressor-Based) Dehumidifiers
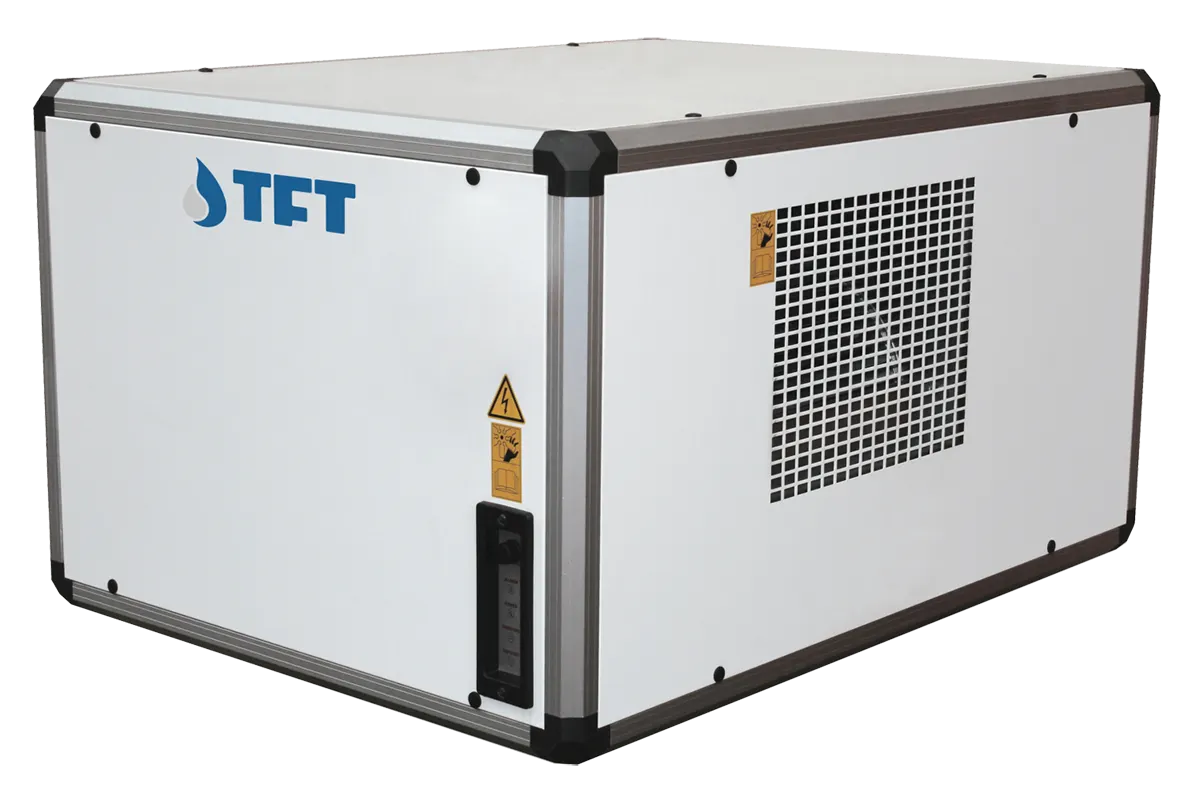
Condensing systems use a refrigeration cycle to condense moisture on a cold evaporator surface. They are efficient at dew-point targets of +10°C and above; the practical lower limit is a dew point of about +5°C. Below that, the evaporator surface drops below 0°C and ices up. When the ambient temperature falls below 15°C, capacity and efficiency also drop markedly. The CD series operates at +10…+40°C ambient and has hot-gas defrost, while catalogue capacities are rated at 32°C / 90% RH. For a 12–14°C kaşar room, the unit must therefore be selected from its low-temperature capacity curve.
In kaşar plants, condensing units are strongest on the fresh-air line, where warm and humid outdoor air is pre-treated, and in surface-drying rooms running close to 15°C.
Silica Gel Rotor (Desiccant / Adsorption) Systems
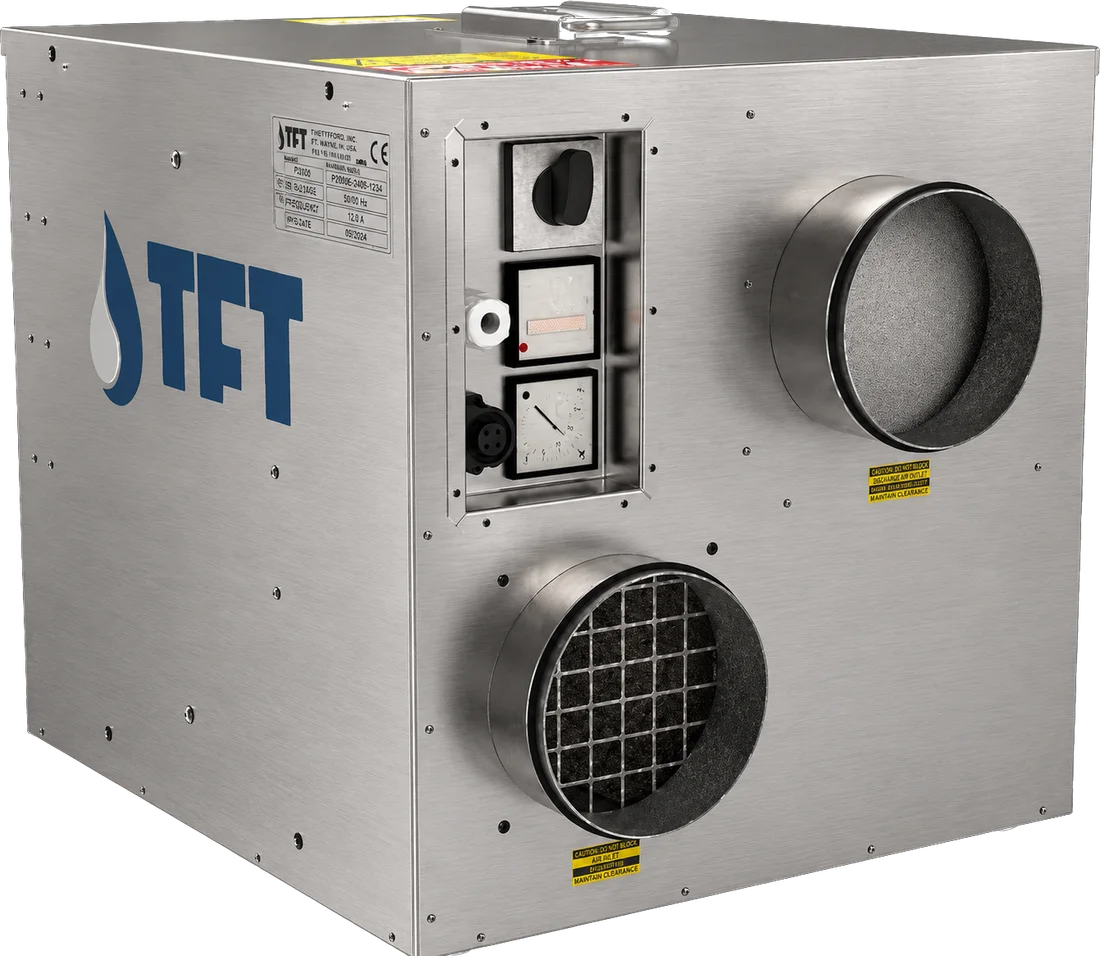
Silica gel rotor dehumidifiers hold moisture by physical adsorption. Process air is dried as it passes through the rotating silica gel rotor, while the rotor's reactivation sector is regenerated with hot air at 100–140°C. These units operate at −20…+40°C ambient, can reach low dew points, and are far less affected by low room temperature than condensing units.
In kaşar plants, a silica gel rotor is a strong option for maturation rooms that run continuously below 15°C. Because the rotor unit adds heat to the room, the room evaporator must be sized for this extra load. Hybrid systems, which combine a pre-cooling coil and a rotor in one casing, use the strengths of both technologies. NKT supplies the ADS, AD, ADP and ADE silica gel rotor series and hybrid systems of the Italian manufacturer TFT – Tecnofrigo Tuscany, for which it is the authorised distributor.
Mould Control, Surface Drying and Listeria Prevention
Microbiological safety is the invisible but most critical function of HVAC design in a kaşar maturation room. Humidity, temperature and circulation directly influence three core microbiological risks: mould growth, Listeria monocytogenes contamination, and surface bacterial biofilms.
Mould Sources and Preventive Parameters
The most common mould genera in maturation rooms are Penicillium, Aspergillus, Cladosporium and Mucor. Growth requires:
- Free surface water: condensation forms when the product surface is colder than the air's dew point (e.g. air at 13°C / 90% RH has a dew point of ≈ +11.4°C)
- High surface water activity; since many Penicillium species grow down to aw ≈ 0.80, RH control alone does not stop mould, it limits growth rate
- Maturation-room temperatures slow mould growth but do not stop it
- Stagnant air (corners with poor circulation)
- Non-hygienic surfaces (wooden pallets, cracked walls, poorly cleaned racks)
The HVAC mould-prevention strategy comprises:
- RH control: 85–90% band during maturation; alarms above 90% and below the drying band
- Continuous air circulation: No dormant zones; fans never switched off
- Surface drying: Controlled drying phase in the first days (≈ 3–7 days); removing free surface water and forming the rind
- Filtration: At least F7 including fresh air, F9 where the risk assessment calls for it; minimises mould-spore ingress
- UV-C sterilization (optional): Installed in the return-air duct; inactivates mould spores, but no direct line-of-sight onto product
- Hygienic design: Coved wall-floor radius, stainless steel shelving, crack-free flooring
Listeria monocytogenes Risk and HVAC Approach
Listeria monocytogenes is one of the most critical pathogens in kaşar production. As a psychrotrophic organism it can multiply even at refrigeration temperatures; it generally needs aw ≥ 0.92 to grow. Under the microbiological criteria of Regulation (EC) 2073/2005 and the Turkish Food Codex, in ready-to-eat foods that support its growth Listeria must be absent in 25 g before the food leaves the producer's control, and must not exceed 100 cfu/g during shelf life.
Surface Maintenance Protocol
- During the first 7 days, inspect kaşar surfaces daily; revisit airflow pattern if local moisture accumulation appears
- At early mould observation, wipe the surface with food-grade brine or a permitted natural antifungal agent (e.g. natamycin within regulated surface limits)
- Before vacuum packaging, perform visual inspection and hardness test
- Batch-level temperature-humidity records retained for the period set in the plant's HACCP procedure
Case Study: 20 Ton/Month Kaşar Maturation Plant (Worked Example)
The following example shows how the moisture load is calculated; every plant should replace the assumptions with its own data. Target output is 20 tons of kaşar per month, block weight 2 kg and, per the producer's recipe, a maturation time of 90 days. Surface drying takes place in a separate room; the calculation covers the maturation rooms.
System Parameters
| Parameter | Value | Notes |
|---|---|---|
| Monthly Output | 20,000 kg | 10,000 × 2 kg blocks/month |
| Maturation Period | 90 days | Producer recipe (the communiqué sets no general minimum for kaşar) |
| Stock in Maturation | ≈ 60,000 kg | 3 months × 20 ton |
| Number of Rooms | 3 parallel rooms | Sequential loading for FIFO |
| Room Volume (each) | 384 m³ | 12 m × 8 m × 4 m |
| Design Point | 12°C / 85% RH | Dew point ≈ +9.6°C; 7.4 g/kg (lower edge of the maturation band) |
| Product Density | ≈ 52 kg/m³ | 20,000 kg / 384 m³ (per room) |
| Fresh Air (per room) | 192 m³/h | 0.5 air changes per hour (assumption) |
| Outdoor Design Condition | 30°C / 70% RH | 18.8 g/kg (assumption) |
Moisture Load Calculation
The total moisture load has four components:
- Product evaporation (Wproduct): Assuming an average daily weight loss of 0.1% (to be verified against the recipe), 20,000 kg × 0.001 = 20 kg/day.
- Fresh air load (Wfreshair): 192 m³/h × 1.2 kg/m³ × (18.8 − 7.4) g/kg ≈ 2.6 kg/h. This load is removed in the central unit on the fresh-air line, before the air enters the room.
- Infiltration (Winfiltration): Door openings and structural infiltration ≈ 2 kg/day (assumption).
- Personnel: 2 persons × 4 hours × 100 g/hour = 0.8 kg/day.
Because the fresh air is treated centrally, each maturation room's unit only handles the product, infiltration and personnel load: 20 + 2 + 0.8 = 22.8 kg/day, or ≈ 28.5 kg/day (≈ 1.2 kg/h) with a 25% safety margin. The central fresh-air unit's load for three rooms is 3 × 2.6 ≈ 7.9 kg/h, or ≈ 9.8 kg/h with the 25% margin. Assigning the same fresh-air load to both the central unit and the room units would count it twice and lead to oversized equipment.
Recommended Configuration
- Central fresh-air pre-treatment: With an outdoor dew point of about +24°C, a condensing unit works efficiently here; the air is dried down to the room dew point (≈ +9.6°C) before distribution. A ducted CD 160-980 model is selected from its capacity curve at the inlet condition.
- Room units: The room is at 12°C, i.e. continuously below 15°C, and its +9.6°C dew point lies in the +5…+10°C intermediate zone. For a load of ≈ 1.2 kg/h per room, a silica gel rotor (ADS / AD series) or hybrid unit and a condensing unit with a verified low-temperature capacity are compared on energy use before selection.
- Cooling: A rotor unit adds heat to the room; the room evaporator is sized for this extra heat load.
- Measurement and control: Relative humidity and temperature are measured at three or more points per room; where possible, humidity is controlled on dew point.
- Humidification: When the product load falls, the cooling coil can over-dry the room and push RH below the band; hygienic steam humidification may then be needed.
Annual energy consumption must be calculated separately from the selected units, local climate data and operating hours. In this example a large share of the dehumidification energy comes from fresh air in summer, so keeping fresh air to what is actually needed is the most effective saving.
Energy Efficiency and Periodic Maintenance
Energy Optimization
A significant portion of operating costs in kaşar maturation plants comes from refrigeration and dehumidification. The main energy-saving approaches are:
- Heat recovery: Plate-frame heat exchanger on the fresh-air intake; recovers heat/cool from the exhaust return air (seasonal effect)
- VFD-driven fans: Variable-speed instead of fixed-speed; significant savings at part load
- Night set-point shift: Loosen RH set-point by ±1% during unattended hours
- Cold storage of vacuum-packed product: Packed cheese exchanges no moisture; the dehumidifier can run at a lower stage
- Keeping fresh air to what is needed: In summer most of the moisture load comes from fresh air
Periodic Maintenance Schedule
| Component | Monthly | Quarterly | Semi-Annual | Annual |
|---|---|---|---|---|
| Air filters (G4, F7, F9) | Visual check | Clean / replace | Full replacement | Class review |
| Evaporator coil | Surface check | Cleaning | Detailed wash | Leak test |
| Condensate drainage | Flow check | Siphon cleaning | Line check | Drain piping inspection |
| Silica gel rotor | — | Visual | Performance test | Wash / seal check |
| RH / Temperature sensors | Data check | Drift check | Calibration | Certified calibration |
| Fan motors | — | Lubrication / check | Vibration test | Bearing replacement (if needed) |
| HACCP documentation | Data archival | Internal audit | External audit | System update |
NKT and TFT – Tecnofrigo Tuscany
NKT – Nem Kontrol Teknolojileri is a supplier of industrial dehumidifiers. For dairy and cheese plants it provides capacity-calculation support for selecting the right unit, technical service and spare parts. Project design, installation and plant automation are outside NKT's scope; they are carried out by the plant's mechanical and automation contractors.
- Unit selection and capacity-calculation support: Choice of technology and model based on room condition, dew point and moisture load
- Equipment supply: Condensing (CD 160-980, CD 1200-3000, CDW 16 / CDK 44-100), silica gel rotor (ADS, AD, ADP, ADE) and hybrid units
- Technical service and spare parts: Maintenance and parts support for supplied units
TFT – Tecnofrigo Tuscany (Italy)
NKT is the authorised distributor in Türkiye for the Italian manufacturer TFT – Tecnofrigo Tuscany. TFT silica gel rotors are supplied in stainless or galvanised steel cassettes with 200 mm and 400 mm depth options and are used in low-temperature maturation and freezer-room applications.
For help selecting the right dehumidifier for your drying and maturation rooms, contact NKT.