Moisture in the Plastics Industry: The Overlooked Cost Factor
In plastic production processes such as injection moulding, extrusion, and blow moulding, moisture is the cause of many quality issues, yet it is often detected too late. Excess moisture in granules entering the production line creates visible defects in the moulded part: silver streaks, bubbles, discolouration, dimensional deviations, and loss of mechanical properties are among the most common.
Moisture-related scrap, reprocessing and customer returns account for a significant share of preventable losses in plastics processing plants; the size of the loss is assessed per site according to material type, process conditions and climate.
Solving moisture problems requires intervention at multiple points along the production line: raw material silo, conveying lines, drying system, injection/extrusion machine, mould zone, and packaging area. Rather than focusing on a single point, a holistic integration map must be considered. TFT – Tecnofrigo Tuscany (Italy) industrial dehumidifiers are used on the air side of this chain, namely the mould zone, silo and conveying air, the production area and the packaging area; moisture inside the granule itself is removed by resin (dry-air) dryers.
Moisture causes damage through two distinct mechanisms in plastics production: hygroscopic plastics absorb moisture into the material structure (internal moisture), while non-hygroscopic plastics experience condensation only on their surfaces (surface moisture). Each mechanism requires a different strategy: internal moisture is removed before processing by resin (dry-air) dryers, while ambient humidity control prevents dried granules from re-absorbing moisture and prevents surface condensation. TFT – Italy dehumidifiers take on this second, air-side task.
Plastic Types and Moisture Behaviour
Hygroscopic Plastics
Hygroscopic plastics have the capacity to absorb moisture molecules into the polymer chain. For these plastics, removing surface moisture alone is insufficient, internal moisture within the granule must also be eliminated. This makes the drying process critically important, and desiccant air dryers are preferred over standard hot-air dryers.
| Plastic | Process | Max. Processing Moisture (%) | Drying Temp. (°C) | Result of Excess Moisture |
|---|---|---|---|---|
| PA6 (Nylon 6) Hygroscopic | Injection | 0.20 | 80 | Silver streaks, foaming |
| PA66 (Nylon 66) Hygroscopic | Injection | 0.20 | 85 | Foaming, part brittleness |
| ABS Hygroscopic | Injection | 0.10 | 80 | Silver streaks, surface roughness |
| PC (Polycarbonate) Hygroscopic | Injection | 0.02 | 120 | Foaming, hydrolysis |
| PET Hygroscopic | Blow/Extrusion | 0.005 | 160–180 | Hydrolysis, IV drop |
| PBT Hygroscopic | Injection | 0.02 | 120 | Hydrolysis, mechanical loss |
| PMMA (Acrylic) Hygroscopic | Injection | 0.10 | 80–90 | Bubbles, optical deviation |
| PE (Polyethylene) Non-Hygroscopic | Extrusion | — | — | Surface condensation → adhesion issues |
| PP (Polypropylene) Non-Hygroscopic | Injection/Extrusion | — | — | Surface moisture → print/label won't adhere |
| PS (Polystyrene) Non-Hygroscopic | Injection/Extrusion | — | — | Surface moisture → aesthetic defects |
Polycarbonate (PC) is one of the most sensitive hygroscopic plastics worldwide. Its maximum processing moisture is 0.02%, a threshold that can be exceeded very quickly upon contact with ambient air. A closed-loop desiccant dryer must be used for PC, and dried material should not be left waiting.
Surface Moisture Management for Non-Hygroscopic Plastics
Non-hygroscopic plastics such as PE, PP, and PS do not absorb moisture structurally; however, condensation can form on their surfaces. This becomes problematic particularly in these situations:
- When granules are transferred from cold storage to a warm processing environment, causing the surface temperature to drop below the dew point
- Condensation forming inside packaging during storage in high-humidity environments
- Surface moisture on PP granules prevents flexographic printing inks and labels from adhering
- Water droplets on PE films cause optical clarity issues
Moisture-Related Production Defects
Surface Defects
When wet granules are injected, water vapour in the melt expands upon reaching atmospheric pressure, leaving characteristic defects on the part surface:
Mechanical Property Loss
Beyond visual surface defects, when hygroscopic plastics (especially PA, PET and PC) are melted without adequate drying, the moisture in the melt breaks polymer chains through hydrolysis; molecular weight falls and the part's strength, impact resistance and elongation are permanently reduced. This loss stems from hydrolysis during processing and cannot be reversed.
It should not be confused with a moulded part taking up moisture from the ambient air afterwards: in a conditioned (moisture-equilibrated) PA6 part, for example, water acts as a plasticiser; hardness and tensile strength drop somewhat while impact resistance and elongation increase. Because the size of the loss depends on the material and moisture level, exact values should be taken from the material manufacturer's data sheet.
Mould Sweating Problem and Dry Air Solution
Psychrometric Explanation: Dew Point and Mould Surface
Mould temperature varies widely with the material and can reach 60–120°C for engineering plastics. Mould sweating is specific to moulds kept at low temperature by chilled water circuits for rapid solidification of the product. The problem occurs when the ambient air dew point temperature rises above the mould surface temperature, condensation, i.e. mold sweating, occurs on the mould.
Example: Ambient 28°C / 75% RH → T_dew ≈ 23.2°C
Chiller water 10°C, mould surface ≈ 15°C — sweating is INEVITABLE.
Solution A: Raise chiller water temp — with 18°C water the mould surface is ≈ 23°C, right at the dew point; to stop sweating the water must be heated further, and cycle time increases!
Solution B: Lower the mould-zone dew point below the mould surface with a TFT – Italy dehumidifier (≤ +10°C for a 15°C mould)
Figure 2: Mould Surface Dew Point Mechanism and Dry Air Solution, Left: Mould sweating is inevitable in humid ambient. Right: Dry air solution with TFT – Italy dehumidifier.
Cost of the Conventional Solution: Capacity Loss
When faced with mould sweating, many operators instinctively raise the chiller water temperature. However, this extends the in-mould cooling time, increasing cycle time and triggering daily capacity loss. The values below are an example based on assumed cycle times of 28 and 34 seconds:
| Parameter | Normal Chiller Water (10°C) | Raised Chiller Water (18°C) |
|---|---|---|
| Cycle time | 28 sec | 34 sec |
| Hourly parts (8-cavity mould) | 1,029 | 847 (≈ 18% fewer) |
| Daily capacity loss (16 hours) | — | ≈ 2,900 parts/day |
| Monthly production loss | — | ~87,000 parts/month |
Dry Air Solution: TFT – Italy Dehumidifier
Supplying dry air from a TFT – Italy industrial dehumidifier to the mould zone lowers the ambient dew point below the mould surface temperature, completely eliminating mould sweating. In this approach, the dehumidifier works with air distribution grilles integrated around the mould:
- Target: Mould zone dew point ≤ mould surface temperature − 5°C (safety margin)
- Technology selection: Based on the target dew point; condensation-type units operate efficiently at targets of +10°C and above, an energy comparison between condensation-type and silica gel rotor units is made in the +5 to +10°C range, and below +5°C a silica gel rotor or Hybrid unit is required
- Capacity: Calculated from the dry-air flow to the mould zone and the ambient moisture load
- Air distribution: Perforated duct or nozzle arrangement uniformly covering the mould surface
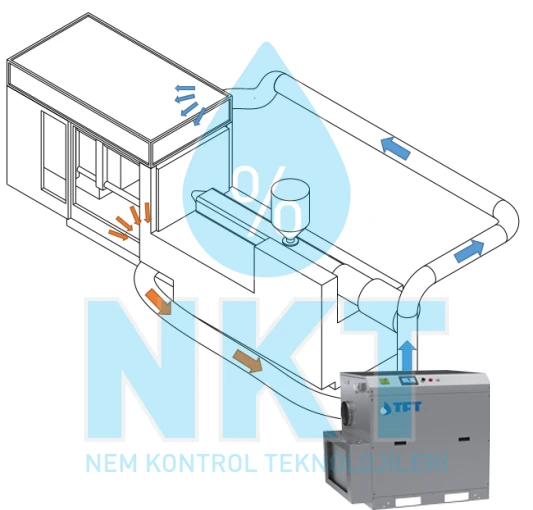
TFT – Italy dehumidifier supplying dry air to the mould zone, fundamentally solves the mould sweating problem.
Special Requirements in IML (In-Mold Labeling) Systems
In IML processes, the label is placed into the open mould by a robotic arm and bonds with the part during injection. In this process, moisture causes two critical problems:
- Label curling: At high humidity, PP or PE labels curl, disrupting robot placement accuracy
- Electrostatic balance: Excessively dry air increases static charge, potentially preventing the label from adhering to the mould. The suitable humidity range is set according to the label and robot manufacturers' recommendations
In IML applications, the outlet airflow rate and dew point of TFT – Italy dehumidifiers must be optimised according to label placement precision. Too low RH disrupts the label's static balance, while too high RH causes mould sweating.
Container Rain (Cargo Sweating)
Container rain is a widespread phenomenon in cargo containers travelling tropical routes, causing serious goods damage. Plastic granules are among the products most affected by this damage.
The mechanism works as follows: During daytime, the container's steel surface heats up from solar radiation, warming the air inside and enabling it to hold more moisture. At night, as the surface cools, air temperature drops and the internal air falls below its own dew point, condensation begins on the steel surface and cargo surfaces.
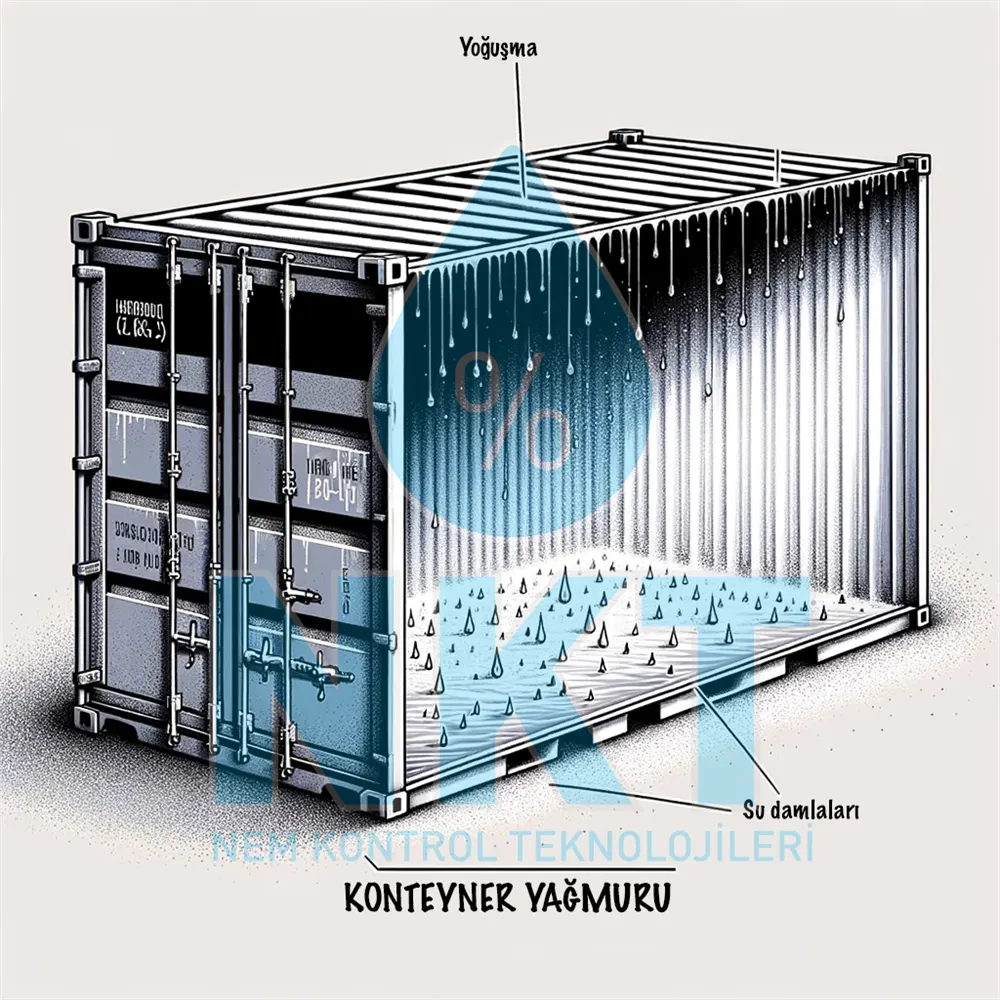
Container rain: Condensation caused by day/night temperature differences settles as liquid on plastic granule surfaces.
Solutions
- In-container desiccant packs: silica gel / calcium chloride packs sized to the container volume, cargo and route
- Active dehumidification unit: active in-container dehumidification solutions for long routes
- Moisture-barrier packaging: Filling granules into low moisture-permeability PE bags
Central Silo Conditioning
Moisture Ingress During Silo Truck Transfer
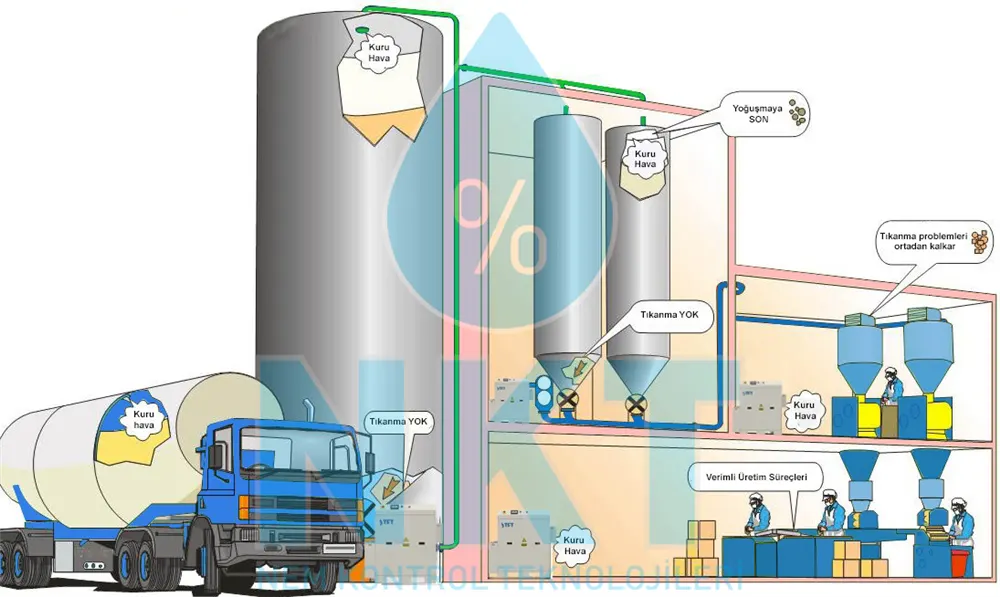
Plastic granules are pumped into silos via silo trucks. A critical issue occurs during transfer: granules are conveyed into the silo using compressed air from the truck, and this compressed air contains moisture. The water vapour sent into the silo along with the moist air disrupts the moisture control regime and causes blockages in the central material conveying system due to day/night temperature differences.
A TFT – Italy industrial dehumidifier, matched in capacity to the silo truck's intake airflow and integrated at the intake point, ensures that plastic granules are transferred into the central raw material silo using dry air.
In-Silo Conditioning
Granule residence times in silos can range from hours to days. During this period, the moisture content of the silo's internal atmosphere is critically important. Particularly for hygroscopic plastics, in-silo air conditions can cause dried granules to re-absorb moisture after leaving the drying oven.
Dried hygroscopic granules (for example PA66) can re-absorb moisture while waiting in a silo or intermediate hopper and exceed the processing moisture limit, which raises the scrap (reject) rate. Supplying dry air to the silo limits moisture re-absorption during the holding time. The required dew point is set by the material's processing moisture limit and the holding time.
Equipment Selection: TFT – Italy Dehumidifiers
When selecting an industrial dehumidifier for plastics production processes, different technologies are preferred depending on the application point. The use of TFT – Italy dehumidifiers by application point is summarised below; resin (dry-air) dryers are not included in this table and are not part of the NKT – Nem Kontrol Teknolojileri product range:
| Application Point | Technology | Target | TFT – Italy Series |
|---|---|---|---|
| Mould zone dry air | By target: condensation, rotor or Hybrid | Dew point safely below the mould surface (e.g. mould − 5 K) | CD / AD / ADP series, Hybrid |
| Silo conditioning | Silica gel rotor | Set by the material's processing moisture limit and holding time | AD / ADP series |
| General production area humidity | Condensation + rotor | 40–50% RH | CD / AD combination |
| Packaging zone | Condensation | 50–60% RH | CD series |
Capacity Calculation Principles
Capacity sizing for TFT – Italy dehumidifiers in plastics production facilities is determined by three main factors:
- Mould zone: Number of machines × required airflow per machine (based on ambient volume and mould temperature)
- Silo conditioning: Silo volume + silo truck transfer airflow + moisture load calculation
- General area: Facility volume × air change rate × target humidity level
NKT – Nem Kontrol Teknolojileri supplies TFT (Italy) silica gel rotor and condensation dehumidifiers for plastics production plants, supports unit selection using space conditions and moisture load, and provides technical service and spare parts. Design, installation and commissioning remain within the scope of the facility's designer and contractor.