Chocolate and confectionery production stands among the most thermodynamically demanding processes in modern food engineering. The crystalline structure of cocoa butter, the surface activity of sugar, and the gloss of enrobed products all rest upon delicate balances that can collapse within a few degrees of temperature or a few grams of moisture. Cooling tunnels sit at the heart of this fragile equilibrium: this is where post-tempering cocoa butter sets in its Beta-V crystalline form, where panned product surfaces acquire their gloss, and where enrobed chocolates become packaging-ready. Yet most producers overlook a critical truth, the success of this stage depends as much on, sometimes more than, airborne moisture management as it does on refrigeration capacity.
In a cooling tunnel the product cools as it travels; its surface reaches its coldest point in the last zone of the tunnel, and the product then leaves the tunnel into the warmer, more humid production hall. If at these points the absolute humidity of the air (in g/kg of dry air) implies a dew point above the product surface temperature, the chocolate surface becomes a condensation surface. This brief moisture deposition forms a microscopic water film, but its visual consequences are permanent: the surface goes matte, gloss is lost, grey-white sugar bloom appears, and the product either loses sales value or is scrapped entirely. This article addresses cooling tunnel dehumidification engineering from a comprehensive perspective, from psychrometric fundamentals and the correct selection and integration logic for silica-gel rotor desiccant systems to a representative worked example for enrobed chocolate.
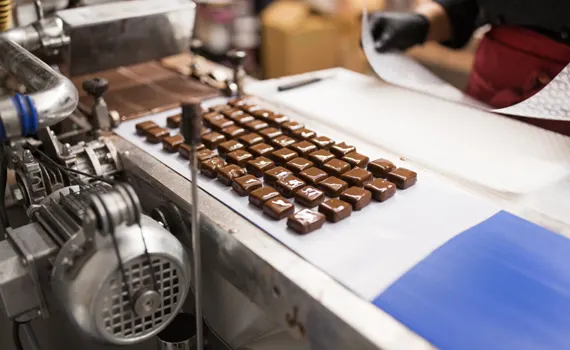
Bloom on Chocolate Surfaces: Origins of Fat and Sugar Defects
The white, grey or matte appearance occasionally visible on chocolate surfaces is the quality defect known industry-wide as bloom. Consumers often interpret this as "staleness", yet bloom is not a microbiological issue but a purely physicochemical surface phenomenon. Two principal bloom mechanisms are recognised in academic literature, and both are directly linked to the cooling tunnel stage.
Sugar Bloom: Directly Moisture-Driven
Sugar bloom forms when sucrose crystals on the chocolate surface come into contact with surface moisture. The mechanism unfolds step by step: in a high-humidity environment or due to condensation in the cold tunnel zones or at the tunnel exit, a thin water film settles on the chocolate surface; in this film the surface sugar crystals dissolve and a saturated sugar solution forms; when the water subsequently evaporates, the dissolved sugar recrystallises, not in its original form but as much larger, disordered crystals. These new crystals scatter light, dulling the chocolate surface and producing the characteristic white layer. The flavour may not change, but visual acceptability is entirely lost.
The critical trigger for sugar bloom is the difference between the product surface temperature and the air dew point. Enrobed chocolate enters the tunnel with a surface temperature of about 28-30°C; this surface is far above the tunnel-air dew point, so no condensation occurs at the inlet. The risk grows as the surface cools along the tunnel: the most critical points are the last zone, where the surface is coldest, and the tunnel exit, where the cold product enters the warmer, more humid hall. The tunnel inlet, by contrast, is the main infiltration path through which humid hall air leaks into the tunnel. Tunnel air is usually held at no more than 50% RH, typically 40-50% RH; the value that governs, however, is a dew point kept at least 3 °C below the lowest product surface temperature. Under this condition surface condensation does not physically occur.
Fat Bloom: Temperature-Fluctuation Driven
Fat bloom originates from instability in the cocoa butter crystalline structure. Cocoa butter exhibits six polymorphic forms (Form I-VI); the glossy, hard, brittle texture of high-quality chocolate is achieved only through Form V (Beta-V) crystals. The tempering process seeks to maximise Form V nucleation in the chocolate mass. The cooling tunnel is the critical stage where this structure is locked in.
If the product surface temperature falls too rapidly inside the tunnel, or if temperature fluctuations occur along its length, cocoa butter shifts to an unstable polymorph such as Form IV; over time, this form converts to the lower-energy Form VI and during this transition liquid fat migrates to the surface, producing the whitish, oily layer. Unlike sugar bloom, fat bloom is not caused by moisture; it is a defect of tempering, temperature profile, crystallisation and fat migration. Temperature uniformity along the tunnel is therefore the main tool for preventing fat bloom.
Surface Defects in Confectionery and Panned Products
Bloom is not exclusive to tablet and enrobed chocolates. Panned (drage) products, hard candy, caramels, jellies, and fondant-filled confectionery are equally sensitive to surface humidity. In panning, the polishing gloss layer remains stable only at about 30-45% RH and 15-22°C; high humidity initiates surface crystallisation and syrup swelling. Hard candies subjected to surface humidity undergo rapid cold flow and tackiness, leading them to adhere directly to packaging and lose shelf life. For these reasons confectionery facilities must apply the same humidity discipline to the post-tunnel holding zone and the pre-packaging buffer zone as they do to the cooling tunnel itself.
Cooling Tunnel Types and Operating Principles
Industrial cooling tunnels are built in different configurations depending on product type, capacity requirement, and line geometry. Designing a dehumidification strategy demands a thorough analysis of the tunnel-specific airflow pattern, opening geometry, and evaporator placement. Three principal types are practically significant.
Linear (Straight-Path) Cooling Tunnels
Linear tunnels are the most widespread configuration, with the conveyor running in a straight line through the tunnel. They are favoured for enrobed chocolate lines, post-moulding tablet cooling, and after-panning drying. Typical lengths range from 10 to 50 metres; examples exceeding 80 metres exist for higher-throughput requirements. Two to four evaporator groups are placed along the conveyor, and airflow is generally counter-flow (against product direction); this ensures the product nearest the tunnel exit encounters the coldest air, securing the final temperature target.
The advantage of linear tunnels from a humidity-control perspective is the predictability and uniformity of the airflow pattern; the disadvantage is that both ends contain product-entry/exit openings, doubling the infiltration load. For chocolate, the typical tunnel temperature is 8-14°C and target RH is 40-50%.
Spiral (Helical) Cooling Tunnels
Spiral tunnels are designed to deliver long residence times within a small floor footprint. The conveyor wraps in a helical pattern around a vertical axis; product ascends or descends spirally while airflow circulates around all product surfaces. They are ideal for products requiring 30-60 minutes of cooling, particularly high-fat enrobed chocolates and filled pralines. Spiral tunnels have only one inlet and one outlet opening, making air-sealing management easier than in linear tunnels; however, the internal volume is much larger and evaporator defrost strategy becomes more complex.
Tunnel-less Cooling Cells and Batch Systems
For small-scale production and specialty items (artisan praline, seasonal packaged chocolate, special-batch production), enclosed cooling cells are used. Unlike tunnels, these systems do not provide continuous flow; trays are loaded, the door is closed, and cooling proceeds for a defined period. From a humidity perspective these systems are the easiest to control because there is no atmospheric mixing other than at door openings; however, each door opening introduces a concentrated moisture load to which the system must react quickly.
| Product Category | Tunnel Type | Internal Temp (°C) | Target RH (%) | Dew Point Target (°C) | Moisture Risk |
|---|---|---|---|---|---|
| Enrobed chocolate | Spiral / Linear | 8 – 14 | 40 – 50 | ≈ −5 … +4 | Very High |
| Tablet & moulded chocolate | Linear | 10 – 16 | 40 – 50 | ≈ −3 … +6 | High |
| Panned drage | Cell / Linear | 15 – 22 | 30 – 45 | ≈ −2 … +10 | High |
| Caramel & hard candy | Linear | 10 – 16 | 40 – 55 | ≈ −3 … +7 | High |
| Praline & filled | Spiral | 8 – 12 | 40 – 50 | ≈ −5 … +2 | Very High |
| Liquorice | Linear / Tunnel | 15 – 20 | 35 – 45 | ≈ 0 … +8 | High |
| Biscuit/cake cooling | Linear | 18 – 24 | 50 – 60 | ≈ +7 … +16 | Medium |
The Mechanics of Condensation in the Cooling Tunnel
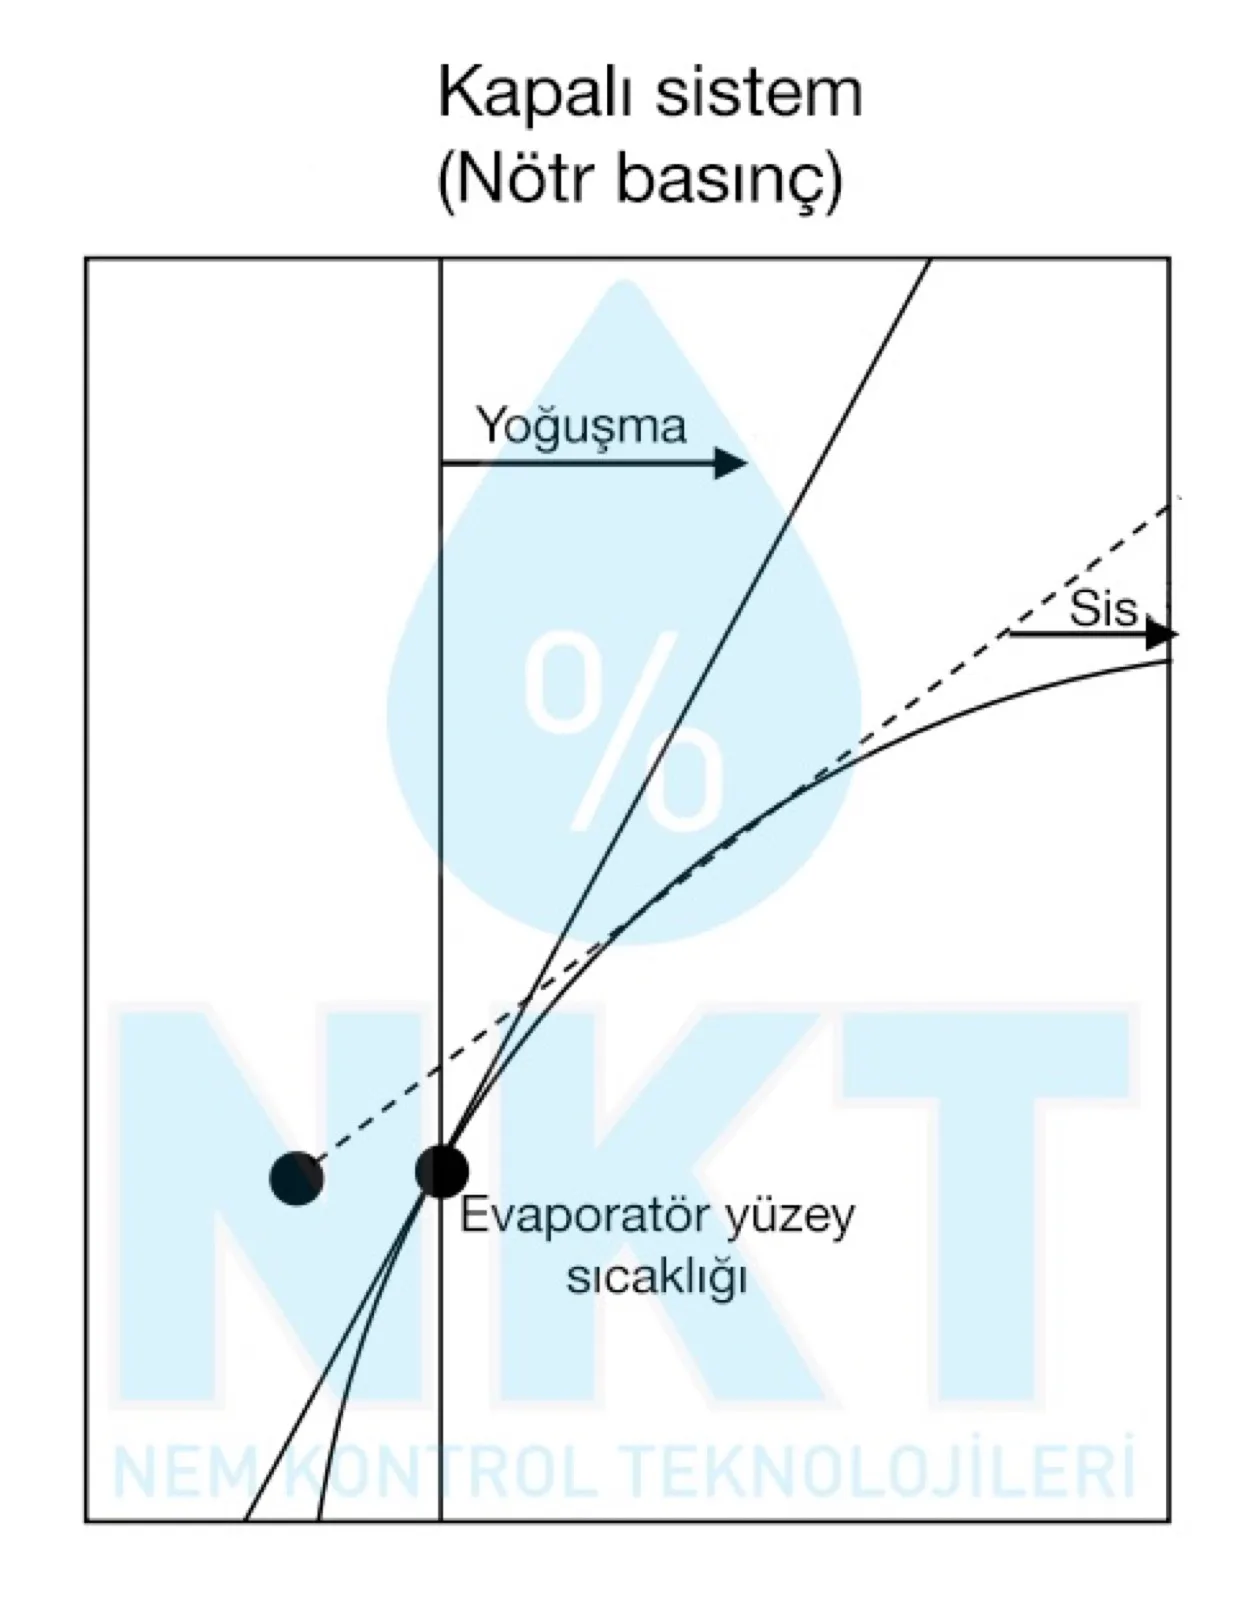
The condensation problem in a cooling tunnel rests on a simple observation: any surface cooled below the dew point of the surrounding air will condense water vapour out of that air. When a warm product (for example enrobed chocolate at 28°C surface temperature) reaches the tunnel inlet, its surface is far above the tunnel-air dew point and no condensation occurs at the inlet; condensing on a 28°C surface would require an air dew point above 28°C. As the product travels through the 8-14°C cold air stream, its surface temperature falls and reaches its minimum in the last tunnel zone. If the air has not been dehumidified sufficiently, condensation starts there, once the surface drops below the air dew point. At the tunnel exit, the cold product meets warmer, more humid hall air; if the hall-air dew point is above the product surface temperature, condensation now forms outside the tunnel.
Several physics laws govern this process. First, the saturation pressure curve: air can hold a temperature-dependent maximum mass of water vapour; as temperature falls, this capacity decreases exponentially. At 30°C, air can carry ~27 g/kg; at 14°C, only ~10 g/kg. Second, absolute-humidity conservation: when a parcel of air is cooled, its absolute humidity content does not change, only its relative humidity rises. Air at 30°C and 60% RH (16 g/kg) cooled to 14°C still carries 16 g/kg, but its RH is now above 100% and the surplus deposits as condensation. Third, the local boundary-layer behaviour: a thin boundary layer forms between the product surface and the air, and condensation occurs there as a microscopic water film.
In practical engineering, the inequality must be reversed: the tunnel air's absolute humidity (w_air) must be lower than the saturation humidity at the product surface temperature (w_saturation). The safety margin is expressed as a dew point: the tunnel-air dew point should be at least 3°C below the lowest product surface temperature. For enrobed chocolate, for example, the surface falls to about 10°C at the tunnel end (w_saturation ≈ 7.6 g/kg); the dew point target is at most +4°C, preferably +2°C, which corresponds to about 5.0 / 4.4 g/kg of absolute humidity.
Infiltration: The Moisture Load Through Openings
The conveyor openings at the tunnel inlet and outlet are the principal pathways through which ambient air infiltrates the tunnel. In most tunnels, infiltration is the largest single item of the total moisture load. Infiltration load is proportional to opening area, indoor-outdoor absolute humidity difference, air density, and the conveyor-induced drag velocity.
Where A is opening area (m²), v is effective air velocity (m/s, typically 0.2-0.5), ρ is air density (≈1.2 kg/m³), w is absolute humidity (g/kg), and the result is the infiltration moisture load in g/hour. As a worked example: outdoor conditions of 30°C and 70% RH (≈18.8 g/kg), tunnel interior 12°C and 45% RH (≈3.9 g/kg), 0.5 m² opening, v = 0.3 m/s. Infiltration ≈ 9,600 g/h ≈ 231 L/day per opening. A single tunnel inlet opening carries an equivalent of roughly 230 litres of water per day in moisture load.
Target Dew Point and Psychrometric Analysis
The success of cooling tunnel humidity control begins with determining the correct dew-point target. Dew point is the temperature at which condensation begins when air is cooled, and it is the direct indicator of absolute humidity. Relative humidity (RH) alone can be misleading because it is temperature-dependent: the same 50% RH means about 13.3 g/kg in summer at 30°C and about 3.8 g/kg in winter at 10°C. In tunnel engineering, using dew point (rather than RH) is the safer reference.
The Product-Surface-Temperature vs Dew-Point Rule
The core rule reads: the dew point of the tunnel internal air must remain below the lowest surface temperature the product will encounter inside the cooling tunnel. This rule is applied with at least a 3°C safety margin. Practical values:
- Enrobed chocolate: Product surface drops to ~10°C by tunnel exit; dew-point target max +4°C, preferably +2°C.
- Tablet chocolate: Surface ~12-14°C; dew-point target max +6°C, preferably +4°C.
- Praline & filled: Surface ~8°C; dew-point target max +2°C, preferably 0°C.
- Panning post-polish: Surface 16-18°C; dew-point target +8°C.
Seasonal Variability and Ambient-Air Influence
Looking at typical moisture loads in Türkiye and other temperate-climate regions, significant seasonal variation is observed. In Istanbul, for example, the summer dehumidification design peak is about 17 g/kg (dew point ≈ 22°C) and the winter average about 4 g/kg; for more humid coastal locations, 32°C and 75% RH (≈ 22.7 g/kg) can be used as a conservative, representative design value. In winter the ambient absolute humidity approaches the tunnel value, so the infiltration moisture load becomes very small; in summer it reaches its peak. System design must size for the worst case (summer peak), while control strategies must operate efficiently at both extremes.
Silica-Gel Rotor Desiccant Dehumidification Technology
Cooling tunnels with a target dew point below +5°C (enrobed, tablet, praline/filled, caramel) require a silica-gel rotor (desiccant/adsorption) or hybrid (pre-cooling + rotor) dehumidification system. Condensation-type units have a practical floor of about +5°C dew point (efficient above +10°C), a limit that is insufficient to prevent moisture-driven sugar bloom for these products. For applications with higher dew-point targets, such as post-polishing dragée or biscuits/cakes, an energy comparison between condensation-type and silica-gel rotor units is made in the +5 to +10°C range; above +10°C, condensation-type units operate efficiently.
Silica-Gel Rotor (Desiccant) Dehumidifier Principle
In silica-gel rotor dehumidifiers, humid air passes through a fluted rotor coated with silica gel or molecular sieve. The rotor rotates continuously; one section adsorbs moisture from the process air while another section is purged with hot regeneration air at 100–140°C. This technology is unmatched in achievable dew point: standard configurations reach -40°C, multi-stage designs can reach -60°C and below. In cooling-tunnel applications such extreme values are rarely needed; however, for enrobed chocolate, praline, and filled product tunnels with dew-point targets around +2 to +4°C, silica-gel rotor systems reach this reliably, whereas condensation-type units cannot.
Advantages of silica-gel rotor dehumidifiers: ability to reach very low dew points, sustained performance at sub-zero temperatures, no evaporator frosting issues, precise dew-point control. Limitations: higher capital cost, regeneration heat requirement (electric/steam/gas), larger physical footprint.
Silica-Gel Rotor: ADS Series (Buffer / Small Capacity)
- Application: Buffer zone, vestibule, pre-pack humidity control, small spiral lines
- Target DP: 0°C to -20°C
- Capacity: 150 – 300 m³/h air flow (ADS 150E-300E); AD series for larger flows
- Strength: Compact rotor, low regeneration load, part-load efficiency
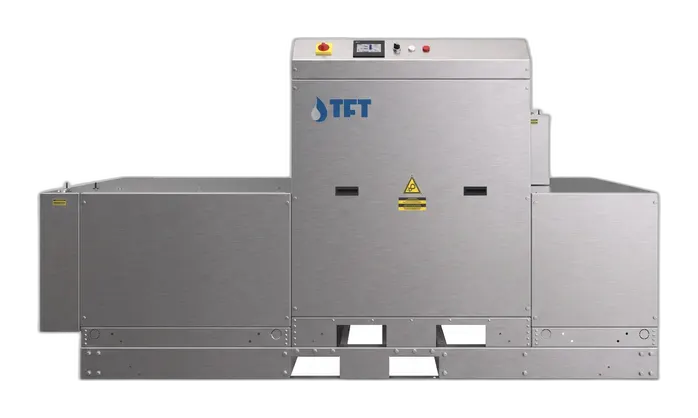
Silica-Gel Rotor: ADP Series (Main Tunnel)
- Application: Enrobed chocolate, praline, filled, low-temperature confectionery main tunnel
- Target DP: 0°C to -40°C
- Capacity: 2,000 – 14,000 m³/h air flow
- Strength: Low DP, sub-zero performance, rotor reliability
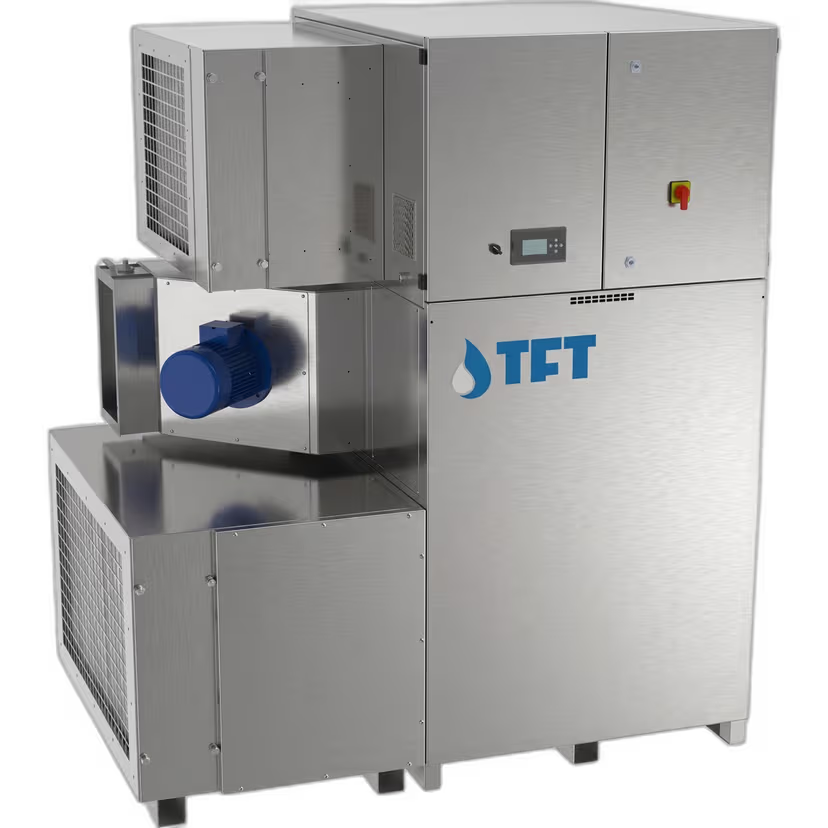
Hybrid Solution for High Ambient Moisture Loads
In coastal facilities where summer ambient air carries high absolute humidity, and in regions with wide seasonal moisture swings, a standalone silica-gel rotor system sees a marked rise in regeneration energy. For these cases a pre-cooling + silica-gel rotor hybrid is used: air is first cooled near the condensation limit by a DX or chilled-water coil, then the silica-gel rotor delivers the target dew point. The unit below integrates both technologies in a single cabinet and reduces regeneration energy under heavy ambient moisture.
System Design: Air Circulation, Buffer Zone, and Filtration
Correct equipment selection alone is not sufficient; the integration of the dehumidifier with the tunnel, air distribution, and operational discipline together determine final performance. A "well-specified but poorly integrated" system can underperform a "moderately specified but well integrated" one.
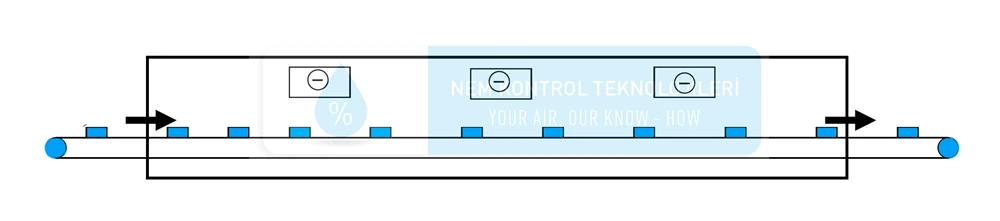
Positive-Pressure Strategy
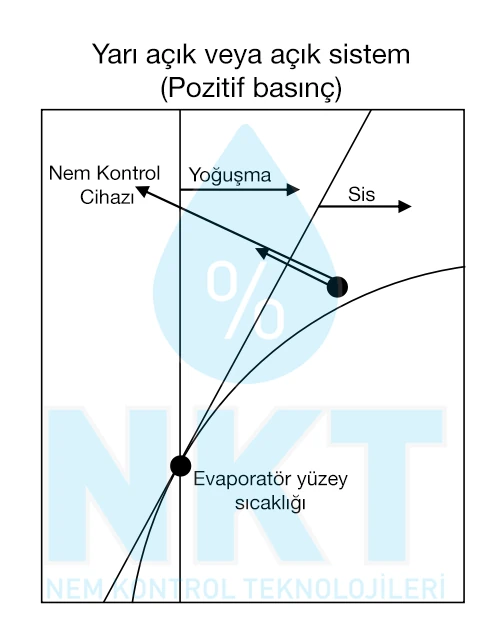
Maintaining the cooling tunnel at +5 to +20 Pa above ambient creates outward airflow at all openings, preventing infiltration. Dry air supplied by the dehumidifier is introduced at the tunnel head or mid-point; this air physically blocks ambient humid air from entering through openings or leakage points. Positive-pressure balance requires regular measurement; excessive positive pressure wastes energy and stresses doors and seals.
Buffer Zone (Inlet and Exit Vestibule) Design
Adding a buffer zone (vestibule) between the cooling tunnel and the general production area makes the humidity transition two-stage. While the production area is typically 22°C and 50-60% RH, the tunnel interior is 12°C and 45% RH. The buffer zone bridges the two environments at 18°C and 45% RH. At the inlet, the buffer zone reduces the leakage of humid hall air into the tunnel. The critical transition, however, is usually at the exit: when product cooled to about 10°C leaves into a 22°C / 55% RH hall, the hall-air dew point is about +12.5°C (+11.1 to +13.9°C for 22°C / 50-60% RH) and moisture condenses on the product surface. An exit/packing buffer zone held at 18°C / 45% RH has a dew point of about +5.9°C and prevents this condensation. The buffer zone should have its own dehumidification system; a small-capacity silica-gel rotor unit (e.g. ADS 150E-300E) handles this duty. This approach reduces the main tunnel dehumidifier load.
Air Distribution and Flow Pattern
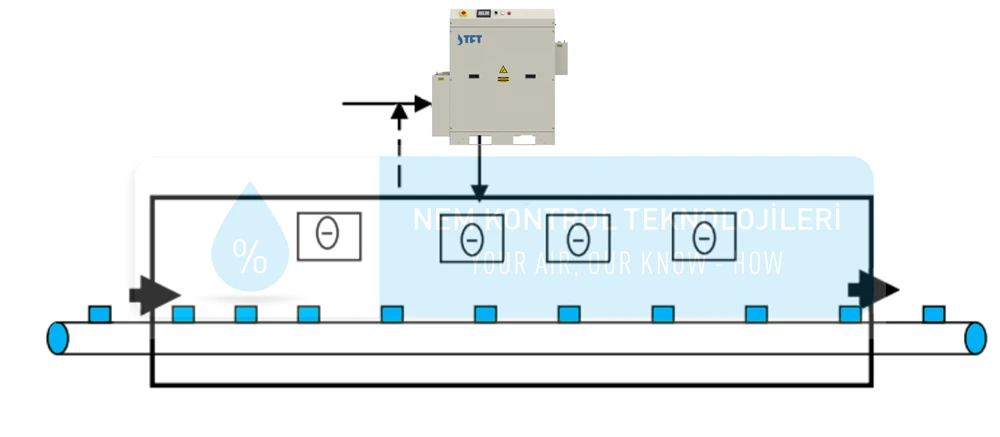
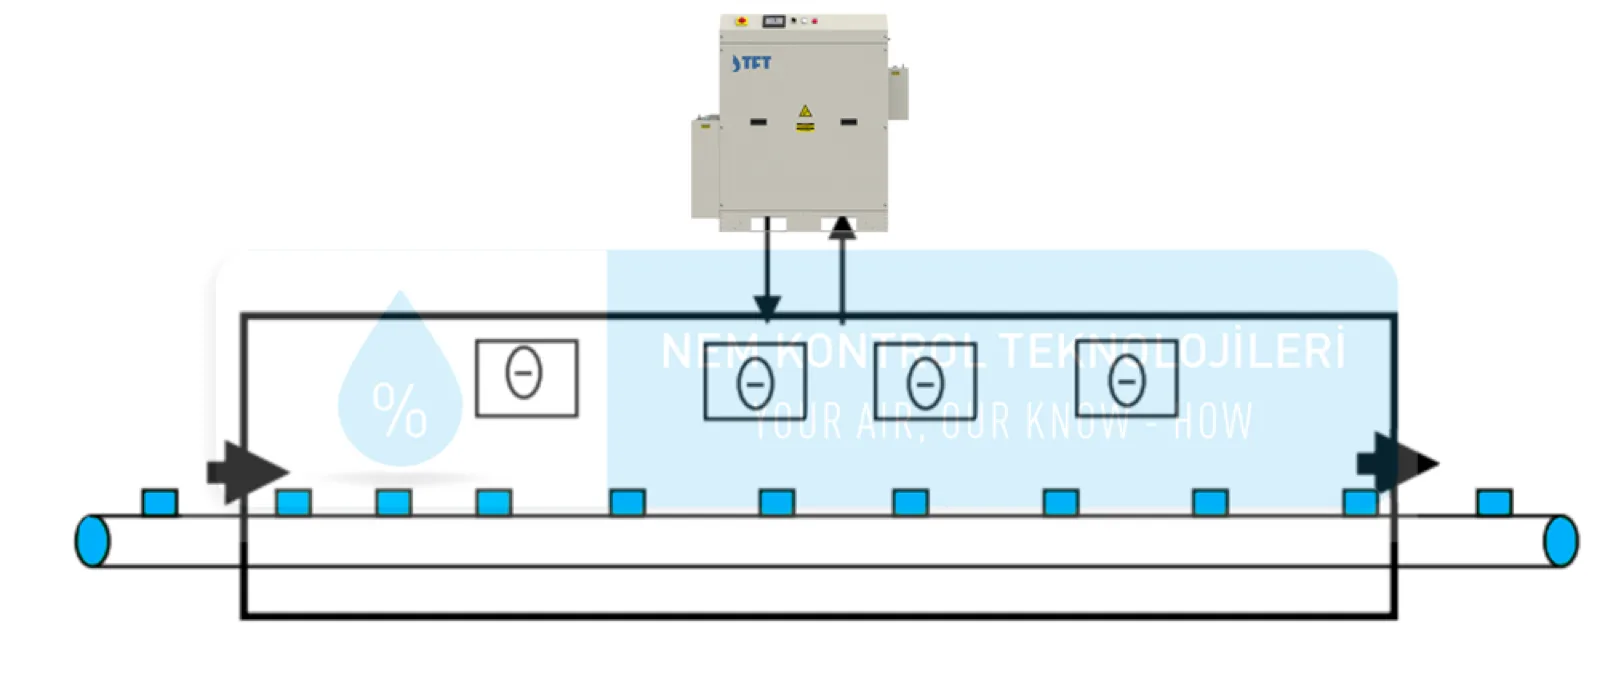
Dry air supplied to the tunnel replaces the resident air through a dilution principle. For effective distribution, perforated ducts or plenum-based multi-point supply should be used rather than single-point injection. Air-change rate is recommended at a minimum of 10-15 ACH for chocolate tunnels, with 20-30 ACH for enrobed lines. Air flow should be counter-flow to product motion; the driest, coldest air should meet product nearest the tunnel exit.
Door and Opening Management
Tunnel inlet/outlet openings are the largest infiltration source. To minimise these openings: PVC strip curtains (rapid-closing plastic strips) are fitted across the conveyor at the exact opening size; air curtains are combined with positive pressure; product entry height is kept minimal. Service doors should be interlocked, one open while the other is locked. This discipline markedly reduces the infiltration moisture load.
Filtration: Food Hygiene and Equipment Protection
For food production filtration serves two purposes: first, preventing dust and particles from settling on the product; second, protecting the dehumidifier rotor/coil from contamination. Standard filtration follows an ISO 16890 chain of ISO Coarse pre-filter + ePM1-class fine filter + ePM1 ≥ 80% final filter (G4 / F7 / F9 in the withdrawn EN 779 classes). For high-hygiene lines, H13 HEPA filtration may be added. Filter replacement intervals must be monitored via differential pressure, with an automatic alert when the threshold is exceeded.
Worked Example: Enrobed Chocolate Line (representative)
The calculation below uses representative values chosen to illustrate the method; it does not describe a specific facility. On a real line the values must be recalculated from the plant's own measurements. Psychrometric values are calculated with the Magnus relation (17.625 / 243.04) at 101.325 kPa.
Design Inputs
| Parameter | Value | Note |
|---|---|---|
| Tunnel | 32 m linear, 3 zones | Conveyor 1.0 m, 3.5 m/min (≈ 9 min residence) |
| Tunnel internal temperature | 14°C → 8°C | Staged cooling |
| Lowest product surface temperature | ≈ 8°C | Tunnel exit |
| Target dew point | ≤ +2°C (≈ 4.4 g/kg) | ≥ 3°C margin to the surface |
| Openings | 2 × 0.4 m² | Effective air velocity 0.35 m/s |
| Summer design ambient | 32°C, 75% RH | ≈ 22.7 g/kg (conservative, representative) |
Moisture Load Calculation
- Infiltration (2 openings): 2 × 0.4 m² × 0.35 m/s × 1.2 kg/m³ × (22.7 − 4.4) g/kg × 3600 ≈ 22,100 g/h
- Personnel and service doors (estimate): ≈ 800 g/h
- Product: Moisture released by the coated product is neglected in this example.
- Design load (including 20% safety margin): (22,100 + 800) × 1.2 ≈ 27,500 g/h ≈ 27.5 kg/h
Required Dry-Air Flow
With supply air at about −20°C dew point (≈ 0.77 g/kg; saturation over water is used), the required dry-air flow is about 6,400 m³/h; if the supply only reaches −15°C dew point (≈ 1.18 g/kg), the flow rises to about 7,200 m³/h. This falls within the ADP 2000-14000 series range (2,000–14,000 m³/h); the exact model, regeneration type and performance are confirmed from the product documentation.
- Buffer zone: For a small vestibule held at 18°C and 45% RH (≈ 5.7 g/kg, dew point ≈ +6°C), the ADS 150E-300E (150–300 m³/h) can be considered; according to the product page its moisture removal is about 0.57–1.1 kg/h. Larger vestibules call for the AD series.
- Pressure and openings: The tunnel is held at +5 to +20 Pa positive pressure, with PVC strip curtains and an air curtain at the inlet.
Energy Efficiency and Periodic Maintenance
The cooling tunnel + dehumidifier combination is among the highest-consuming systems in a modern food production facility. It accounts for a significant share of the plant's energy consumption. Sound design decisions and disciplined operations can reduce this share significantly.
Energy-Optimisation Strategies
- VFD for fan and compressor control: Variable-frequency control matched to production rate yields marked energy savings at partial load (fan power varies roughly with the cube of airflow).
- Synchronisation: The dehumidifier should turn off when the tunnel stops; it should also be activated 15-30 minutes before tunnel start to bring the environment to target.
- Waste-heat recovery: Heat rejected from the cooling-tunnel condenser can pre-heat the silica-gel regeneration air and reduce regeneration energy.
- Night/weekend mode: Outside production hours, target dew point can be relaxed (for example from +4°C to +6°C) and airflow reduced, lowering energy consumption.
- Buffer-zone approach: The main tunnel's moisture load drops with a buffer zone.
- Smart control: Setpoint optimisation tied to seasonal ambient data reduces annual energy consumption.
Periodic Maintenance Schedule
| Frequency | Action | Purpose |
|---|---|---|
| Daily | Drain line check, dew-point measurement, pressure-difference monitoring | Early detection of blockage and drift |
| Weekly | Tunnel interior cleaning, drain siphon flush, door/curtain mechanical inspection | Hygiene, seal integrity |
| Monthly | Pre-filter replacement (ISO Coarse / G4), evaporator coil cleaning | Airflow preservation, heat-transfer efficiency |
| Quarterly | Fine and final filter replacement (F7/F9), rotor seal inspection, sensor calibration | Dew-point accuracy, performance preservation |
| Half-yearly | Compressor function test, regeneration heater cleaning, comprehensive system analysis | Mechanical health, energy efficiency |
| Annual | Full CIP cleaning, ductwork biofilm testing, rotor performance test, leakage test | Food hygiene certification, long service life |
Maintenance Discipline and Performance Preservation
Neglecting maintenance lets filter loading, seal wear and rotor fouling erode system performance over the years. Disciplined maintenance, in contrast, keeps the system running close to its design performance for many years. This represents a critical difference for investment amortisation.
NKT – Nem Kontrol Teknolojileri
NKT – Nem Kontrol Teknolojileri is the Turkish supplier of silica-gel rotor and Hybrid dehumidifiers made by TFT, Tecnofrigo Tuscany Srl (Italian industrial dehumidifier manufacturer). Our scope is equipment supply, technical support in equipment selection, technical service and spare parts; the design, installation and commissioning of the cooling-tunnel integration are the responsibility of the facility's designer and contractor.
- Selection support: Help in identifying a suitable model across the ADP, AD and ADS ranges from the airflow, target dew point and moisture load provided by the facility
- Equipment supply: TFT silica-gel rotor and Hybrid dehumidifiers
- Technical service and spare parts: For the units we supply