Jelly and gummy confectionery represents one of the fastest-growing segments of the global candy market. Whether built on pectin, gelatin, or agar, these products derive their colour, texture, gloss, chew, and shelf life almost entirely from a single late-stage step on the manufacturing line: the conditioning room. Following cooking and the mogul deposit operation, this stage removes excess moisture in a controlled fashion, stabilises the gel network, and brings each piece to its target water activity (aw). Most observers see only "drying", but in engineering reality, jelly conditioning is an advanced psychrometric problem, because pectin, starch, glucose syrup, and gelatin each follow distinct equilibrium curves with the surrounding air.
What makes the conditioning room uniquely sensitive is that the product is essentially left alone here, with success determined entirely by ambient conditions. After being deposited hot into starch-lined mogul trays, the gummy mass slowly releases moisture into the surrounding air over hours. If room humidity is held too high, the starch stays wet, products stick, and a dull surface bloom forms; if it is held too low, surface case hardening, shrink marks, and visual defects appear. As NKT – Nem Kontrol Teknolojileri, we have prepared this guide to walk through the engineering principles, equipment-selection logic, and the most common field-level mistakes we encounter in jelly and gummy conditioning operations.
Jelly Production Process and the Role of Conditioning
The jelly/gummy production line breaks into five major stages: raw-material preparation, cooking, mogul deposit (moulding), conditioning, and finishing (oiling, coating, packaging). All five contribute to product quality, but the conditioning room is both the longest and the stage where the smallest deviation in ambient conditions is felt most directly in the final product. During cooking, the syrup is boiled at 105–115°C until it reaches its target Brix value, typically 75–82 Brix solids. The hot mass is then cooled to 65–70°C and discharged through the mogul depositor's nozzles into starch-lined trays. A modern mogul line operating at full pace deposits 600–1,200 kg of product per hour into trays — but at this point the mass still contains 18–26% moisture by weight. The final target of 14–16% is reached only inside the conditioning room.
Conditioning lowers aw in the product matrix, which delivers both microbiological stability and the desired textural properties. The critical concept here is water activity (aw): not the total moisture content of the product, but the degree to which water is free to migrate from the product matrix into the surrounding air. Most bacteria cannot grow below aw 0.90 (S. aureus down to about 0.86); most yeasts stop at about 0.88 and most moulds at about 0.80. Xerophilic moulds and osmophilic yeasts, however, can grow down to values close to 0.60, and these are the main risk in confectionery. The target window for jelly/gummy products is therefore aw 0.55–0.70. To reach this window, the surrounding air's vapour pressure must remain below the product surface's vapour pressure — in plain terms, the conditioning room air must be drier than the product surface itself. At 28°C and aw 0.65 the product's surface vapour pressure is roughly 24.5 mbar, while a 28°C / 30% RH room has a vapour pressure of just 11–13 mbar. This sustained pressure gradient is what drives moisture out of the product, day and night.
Conditioning Room Design Parameters
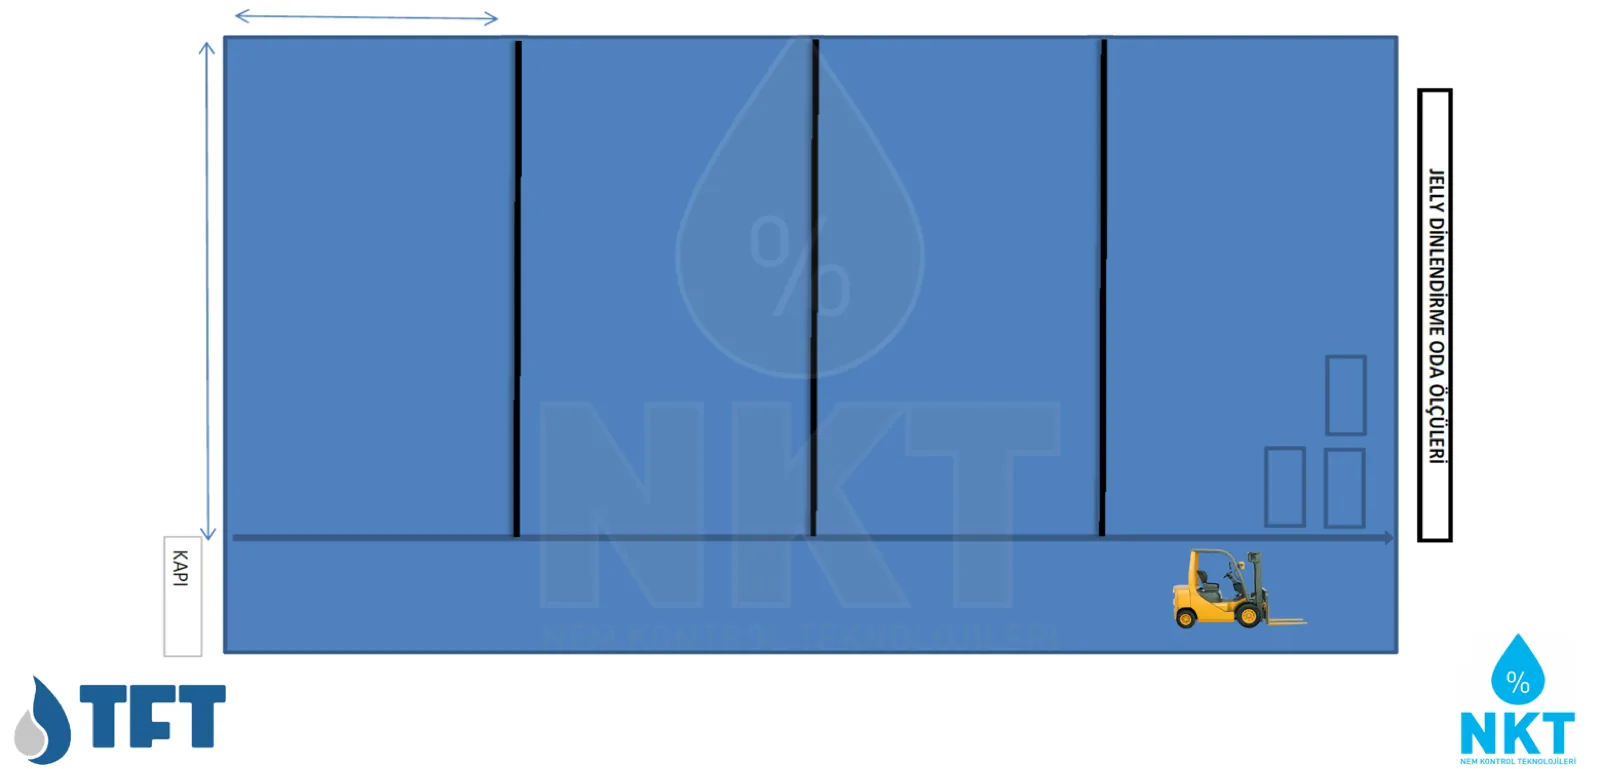
Engineering a jelly conditioning room starts with a small set of decisions: total room volume, trolley count, tray density, air circulation strategy, pressure balance, and door management. These parameters all feed into the moisture-load calculation and ultimately collapse into one number — the kilograms of water per hour that must be removed from the room. The most common design failures occur in rooms that pack in too many trolleys, undersize the airflow, or rely on a single dehumidifier with no redundancy.
Volume, Trolley Density, and Layout
A typical industrial gummy conditioning room is built as a modular space with two rows of mogul trolleys, a central walkway, and distribution panels lining the walls. A single mogul trolley carries 80–130 trays on a 6–8 tier rack, with each tray holding 3–5 kg of starch and 2–3 kg of freshly deposited product. A 25-trolley section therefore contains roughly 10 tons of starch, and a four-section, 100-trolley conditioning room roughly 40 tons — a massive thermal and moisture buffer that explains why the room's humidity reacts so slowly to setpoint changes. Maintain a minimum 60–80 cm spacing between trolleys, plus 25–35 cm of free air space below and above the trolleys. Without these clearances, the bottom trays over-dry and the top trays under-dry; the resulting aw spread within a single batch can reach 0.08, which translates to visible quality variation.
Air Circulation and Pressure Balance
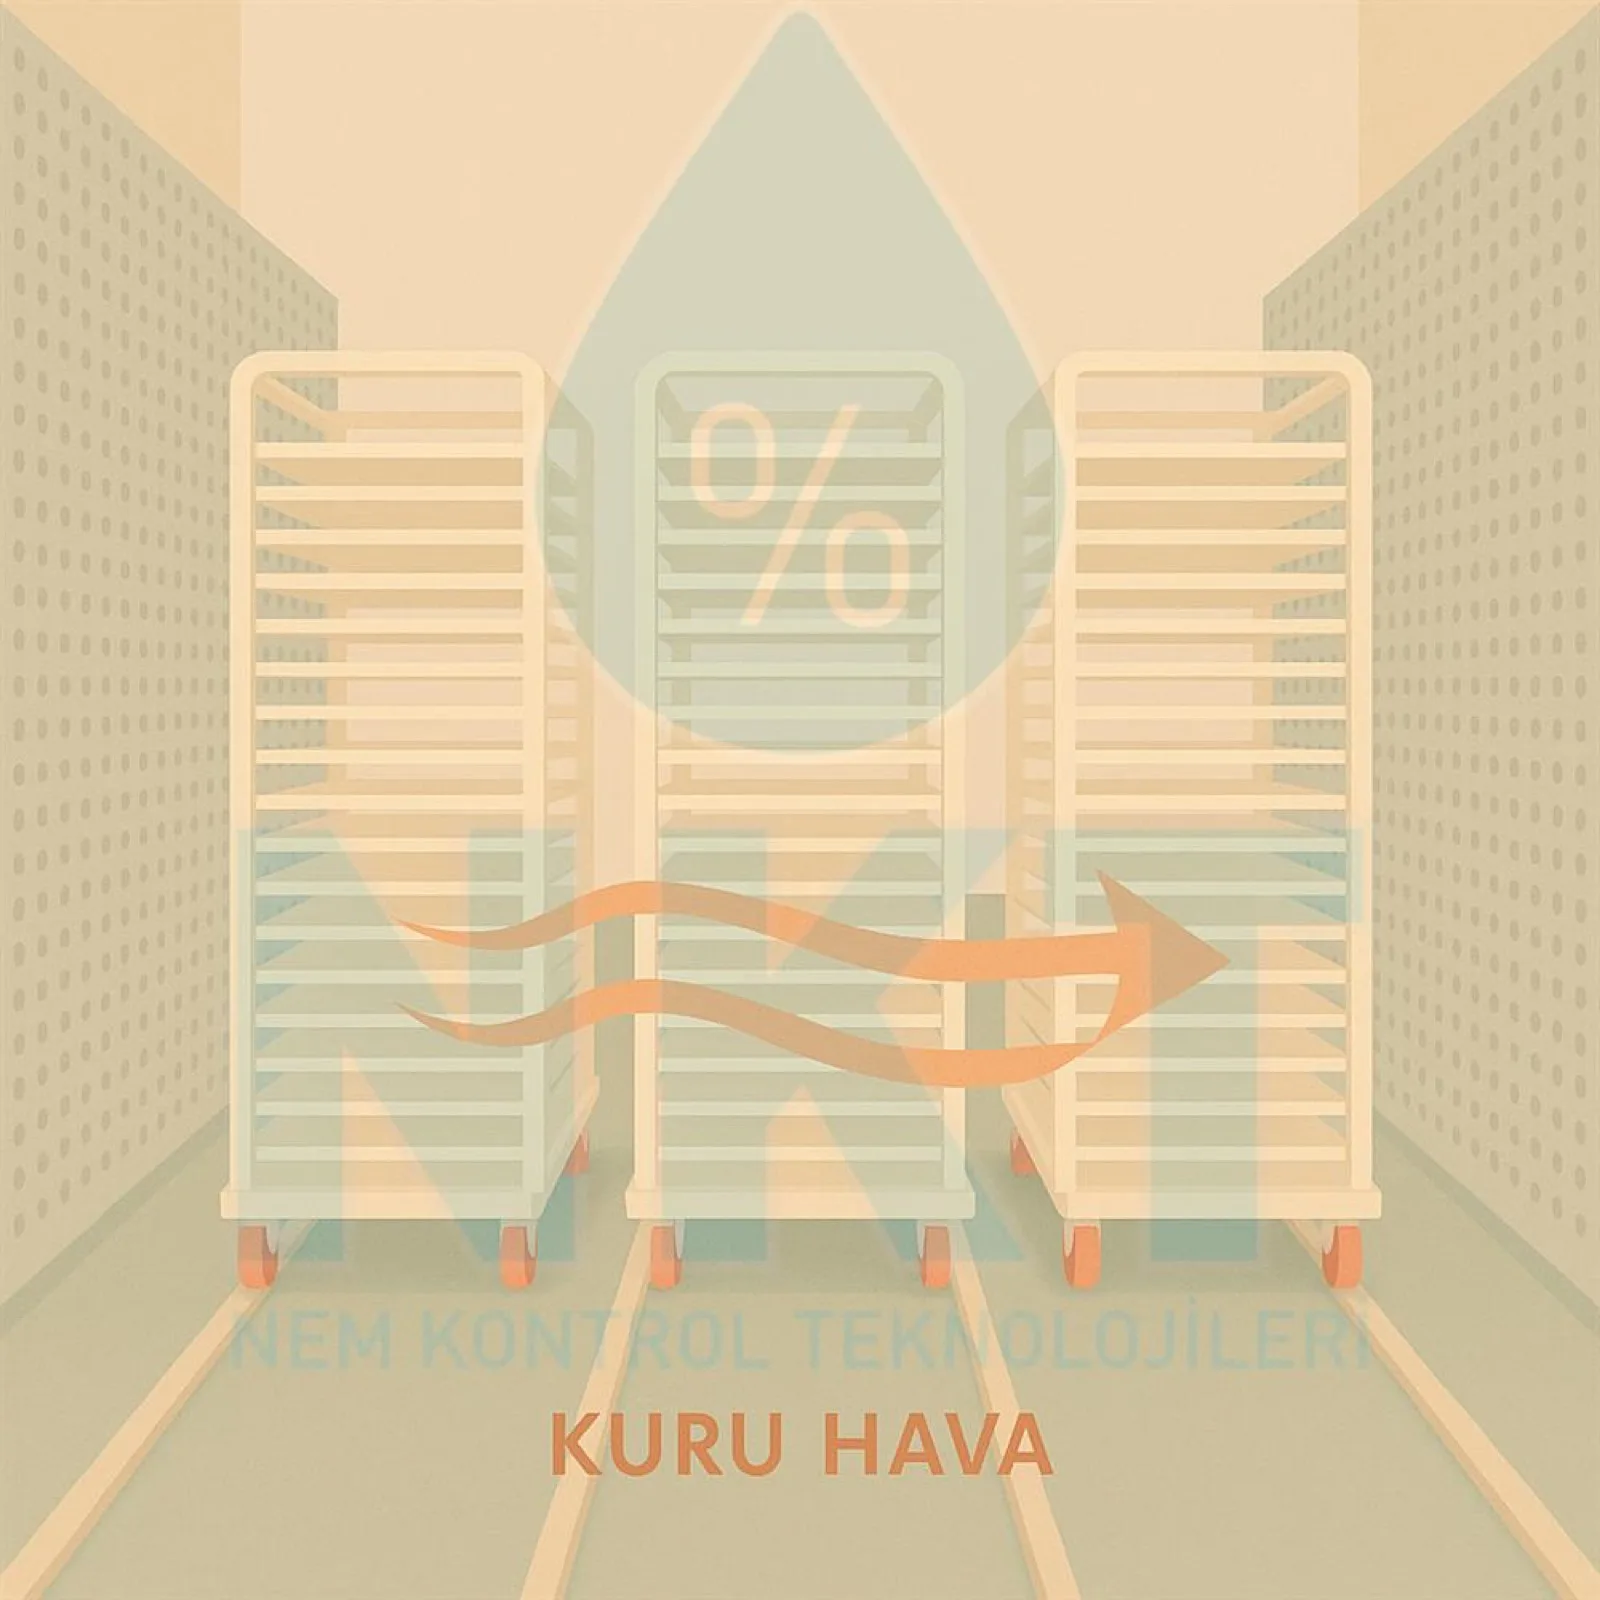
The preferred circulation configuration in modern jelly conditioning rooms is top-return + bottom/side-supply. Warm, moisture-laden air rising from the trays is drawn into a ceiling return plenum, processed through a silica-gel rotor dehumidifier, optionally trimmed for temperature through a heating/cooling coil, and redistributed through floor or side-wall distribution panels. Air-change rate (ACH) is typically 15–25 room volumes per hour; lightly loaded layouts can hold 15–18, but densely packed 130-tray-per-trolley layouts should not drop below 22–25. Local air velocity at the tray surface should sit between 0.3 and 0.8 m/s and should never exceed 1.2 m/s anywhere in the room. Above this threshold, "starch blowback" begins — starch fines lift off the trays, foul filters, contaminate ducts, and degrade rotor performance.
For pressure balance, the conditioning room is held at slightly positive pressure (+5 to +10 Pa) relative to the surrounding corridor. When a door opens or a trolley enters, dry room air then flows out instead of humid corridor air flooding in. Negative pressure is considered only in special cases where the corridor is also kept dry or starch dust must be kept from migrating into adjacent areas. A 2.2–2.5 m air curtain and tight door seals reduce moisture transfer from the corridor into the room.
Moisture Load and Engineering Calculation
Correctly sizing the dehumidification equipment requires a careful estimate of the room's hourly moisture load — the kilograms of water per hour that must be removed from the air. This load has four components: moisture released by the product, equilibrium-moisture shifts in the starch bed, infiltration and makeup-air load from outside, and sensible/latent load from personnel and lighting. The dominant component is almost always product evaporation, since it scales directly with production capacity and cannot be designed away.
Here Mproduct is the total product mass simultaneously present in the room, ΔXproduct is the gap between initial and target moisture content (kgwater/kgproduct), and tconditioning is the time available to reach the target. For a 50 ton/day plant on a 48-hour conditioning cycle with ΔX = 0.07 (i.e. 22% → 15% moisture), product-side moisture load works out to roughly 145 kg/h. Add makeup-air, infiltration and personnel/lighting loads, and the dehumidifier should be specified to a design load of at least 200–230 kg/h. This margin is precisely why the industry rule of thumb — "size the unit to about 1.5 times the calculated product load" — remains good engineering practice.
| Component | Typical Range (50 t/day plant) | Share of Total |
|---|---|---|
| Product evaporation | 120–160 kg/h | ~60–70% |
| Makeup air load | 30–55 kg/h | ~15–25% |
| Infiltration (doors / trolleys) | 15–30 kg/h | ~8–12% |
| Personnel + lighting | 4–8 kg/h | ~2–4% |
| Starch equilibrium shift | 3–7 kg/h | ~2–3% |
| Design total moisture load | 200–230 kg/h | 100% (with margin) |
Target Humidity and Temperature Ranges
The "right" temperature/humidity combination for a jelly conditioning room depends on the product matrix and hydrocolloid type. The reference ranges below summarise widespread industry practice and align with ASHRAE Handbook (Refrigeration, Chapter 42) recommendations and confectionery-engineering literature. As NKT – Nem Kontrol Teknolojileri, the two field problems we encounter most often are: (a) running gelatin gummies on the same room as pectin jellies without separating their cycles, and (b) driving the RH setpoint too low — under the misguided assumption that "drier is always better" — and triggering surface case hardening as a result.
| Product Type | Target Temperature | Target RH | Target aw | Conditioning Time |
|---|---|---|---|---|
| Pectin Jelly | 24–26°C | 28–32% | 0.60–0.68 | 24–36 h |
| Gelatin Gummy | 22–26°C | 28–32% | 0.55–0.65 | 48–72 h |
| Agar-Based | 20–24°C | 30–35% | 0.62–0.72 | 20–30 h |
| Starch Jelly | 25–30°C | 32–38% | 0.65–0.72 | 48–72 h |
| Sugar-Free Gummy (isomalt/maltitol) | 20–24°C | 22–26% | 0.50–0.60 | 36–48 h |
| Sugar-coated (sanding) | 24–28°C | 30–35% | 0.58–0.65 | 24–48 h |
The single most common reference setpoint across the industry is 28°C / 30% RH; at this point dew point sits around +8.8°C and absolute humidity is approximately 7.0 gwater/kgdry air. Achieving the same ΔX at 22°C / 30% RH stretches the cycle by roughly a factor of 1.4. Conversely, raising the room to 30°C / 30% RH shortens the cycle but raises the risk of surface crusting, aroma loss and product deformation. This is why 28°C / 30% RH is widely treated as the "sweet spot" for jelly conditioning.
Operators often act on the assumption that "drier is better" and pull the RH setpoint down to 22–25%. This drives surface moisture out of the matrix far faster than the interior can re-equilibrate, triggering case hardening. The end result is a hard, sealed outer shell with a sticky, wet core — both visually and texturally outside saleable quality. Outside of sugar-free formulations, dropping below 28% RH rarely improves outcomes.
Pectin/Starch Interaction and Moisture Behaviour
The two structural elements that most strongly govern moisture balance in the conditioning room are the pectin (or gelatin) gel network and the starch bed in the trays. High-methoxyl (HM) pectin builds a gel network that depends on high sugar concentration and low pH, while low-methoxyl (LM) pectin gels via calcium bridges. Pectin's moisture-release behaviour is balanced between surface and interior, but if the room RH is held too low, interior-to-surface re-equilibration cannot keep pace and surface cracking begins.
Starch behaves more subtly. Corn starch (the most common moulding starch in mogul lines) enters the system at 7–9% moisture and absorbs both heat and a small amount of moisture on contact with the hot product. Throughout conditioning, the starch acts as the room's moisture buffer: if the room becomes too dry, the starch bed begins to release moisture back into the product; if the room becomes too humid, the starch begins to draw moisture from the product surface. This buffering is exactly why instantaneous responses to RH-setpoint changes appear so slow. A typical mogul-equipped conditioning room contains 25–40 tons of starch; for every 1% RH change in the equilibrium condition, roughly 40–80 kg of moisture migrates into or out of the starch. A 4-unit deviation from 28% RH to 32% RH therefore ties up around 160–320 kg of additional moisture in the starch mass over time — a buffer no dehumidifier can follow instantly.
Gelatin-based formulations operate within a wider RH window than pectin, but gelatin gels release moisture more slowly, which is why gelatin gummies require longer cycles (48–72 hours). The terms "jelly" and "gummy" are sometimes used interchangeably, but from an engineering standpoint pectin jelly reaches target conditions in 24–36 hours while gelatin gummy requires 48–72 hours. If both are processed in the same room, the room must be designed around the worst-case product — or, ideally, the lines should be physically separated.
Silica-Gel Rotor Dehumidification: Why Condensation Type Struggles
This is where the most consequential engineering decision is made: which type of dehumidifier should the room be equipped with? The industry offers two technologies — condensation-type (refrigerant cooling) and desiccant-type (silica-gel rotor). Both have legitimate applications, but for a jelly conditioning room operating at 30% RH and below at 28°C (dew point +9°C and below), the condensation type moves outside its efficient zone.
Condensation Type (Refrigerant)
- Practical dew point floor: ~+5°C; efficient zone +10°C and above.
- At 28°C a +5°C dew point corresponds to about 23% RH and +10°C to about 32% RH; a 30% RH target lies in the defrost and low-COP zone.
- In this zone capacity and COP drop and defrost cuts in; a narrow band is hard to hold.
- Performance degrades visibly during summer months.
- Lower capital cost, but inadequate for the process.
Silica-Gel Rotor (Desiccant)
- Achievable dew point: down to about -60°C.
- At 28°C ambient, stable supply at 15% RH or below is achievable; 30% RH setpoints are easily held.
- Performance is independent of outdoor air temperature.
- Modular design: 2,000–14,000 m³/h capacity range.
- Higher capital outlay, but the correct and sustainable solution for the process.
A silica-gel rotor dehumidifier works on adsorption: water-vapour molecules in the air are bound to the surface of silica-gel-coated channels mounted on a slowly rotating wheel. As the rotor turns, an adsorption sector captures moisture from the process air, while a separate regeneration (reactivation) sector uses 100–140°C hot air to drive the captured moisture out of the rotor and exhaust it from the building. The cycle then repeats. The key advantage is that this process delivers very low dew points independently of ambient temperature — the inverse of condensation cooling, whose efficiency drops as ambient temperature falls. For jelly conditioning, NKT – Nem Kontrol Teknolojileri supplies the ADP series silica-gel rotor dehumidifiers manufactured by the Italian manufacturer TFT – Tecnofrigo Tuscany Srl. The ADP series offers stainless-steel construction, PLC control, and modular steam/electric/gas regeneration options — meeting the hygiene requirements of the food sector.
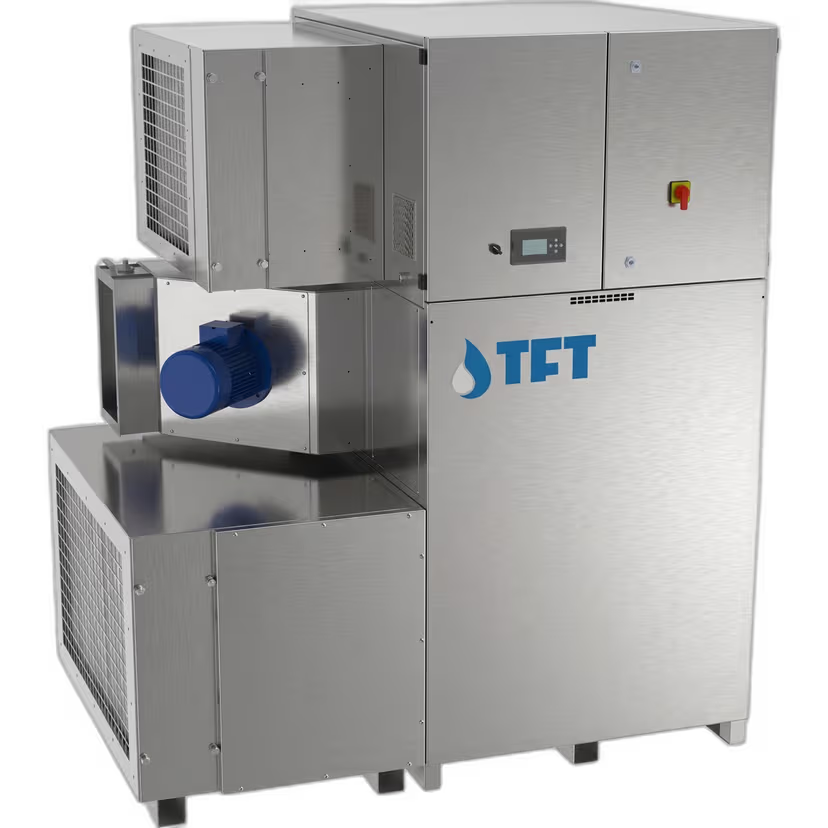
The ADP series dual-rotor configuration is particularly preferred for summer operation or for plants in humid climates (Black Sea region, Marmara coast, humid Mediterranean lowlands). The first rotor pre-dries the makeup-air stream; the second rotor pulls it down to the final dew point. This arrangement splits a high moisture load into two stages and provides redundancy against rotor-ageing performance loss. On the filtration side, the standard build uses a G4 pre-filter plus an F7 fine filter; an additional F9 stage is recommended in environments with significant starch dust load.
Worked Example: 100-Trolley (≈ 16–32 Ton/Day) Jelly Production Plant
The hypothetical case below represents a mid-to-large gummy plant. The plant has a single large conditioning area subdivided into 4 sections; each section accommodates 25 mogul trolleys, and each trolley carries 130 trays. Total tray capacity per room is 4 × 25 × 130 = 13,000 trays. With an average of 2.5 kg of product per tray, each conditioning cycle holds about 32.5 tons of product simultaneously; with a product-dependent conditioning time of 24–48 hours, real daily output is approximately 16–32 tons/day.
Sizing Steps
Representative example (hypothetical plant data):
| Parameter | Value | Notes |
|---|---|---|
| Daily production capacity | ≈ 16–32 tons/day | Mixed pectin jelly + gelatin gummy; depending on 24–48 h conditioning time |
| Number of sections | 4 sections | Each with its own distribution panel |
| Trolleys per section | 25 trolleys | Two rows; 100 trolleys in total across four sections |
| Trays per trolley | 130 trays | 8-tier rack, 16–17 trays per tier |
| Total room volume | ~3,200 m³ | 40 m × 16 m × 5 m net |
| Air-change rate | 22 ACH | ~70,000 m³/h total airflow |
| Target conditions | 28°C / 30% RH | Dew point ~+8.8°C, AH ≈ 7.0 g/kg |
| Design moisture load | ≈ 140 kg/h | Product load 32.5 t × 0.07 / 24 h ≈ 95 kg/h (shortest cycle); ≈ 1.5 × product load including makeup, infiltration, personnel and starch loads plus margin |
| Required dried-air flow | ≈ 22,000 m³/h | Unit outlet ≈ 1.6 g/kg (-10°C dew point); Δx ≈ 5.4 g/kg → 140 / (1.2 × 5.4) |
| Example unit arrangement | 3 × ≈ 12,000 m³/h (ADP 2000-14000 series) | Two duty + one standby (N+1): 2 × 12,000 = 24,000 m³/h covers the requirement with ≈ 10% margin; all three together (36,000 m³/h) give ≈ 65% extra capacity for the shortest cycle and fresh-batch loading peaks |
The most critical decision in this kind of design is "one large unit, or several mid-sized units?" Several mid-sized units are generally the better choice. Distributing the load across 3 × ≈ 12,000 m³/h units rather than one large block keeps production running when any one unit goes offline for service, and gives independent control over local moisture-load variation between sections (a section that has just been loaded with fresh batches always has higher moisture demand than a section near end of cycle).
Performance Verification
At hand-over of the conditioning room, the fluctuation of room RH and temperature, aw measurements at tray level, recovery time to setpoint after door openings and the dew point at the unit outlet should be recorded over a defined period and verified. Acceptance criteria are set by the product recipe and the plant's quality requirements; verification is carried out by the facility's contractor and quality team.
Energy Efficiency and Operational Recommendations
Conditioning rooms are among the largest energy consumers in a jelly plant. The bulk of this consumption is split between rotor-regeneration heating and circulation fan motors. Both of these are accessible to significant savings in a properly designed system.
Regeneration Heat Recovery
The regeneration sector of a silica-gel rotor dehumidifier operates at typically 100–140°C. After leaving the rotor, the exhaust air still carries 60–85°C of usable heat — energy that is wasted if dumped directly to atmosphere. Modern ADP series units offer optional plate heat exchangers that recover part of this exhaust heat by pre-heating the incoming regeneration air and reduce regeneration energy; payback is calculated from the plant's energy prices and operating hours.
Night/Weekend Mode and Holiday Schedule
During production downtime — for plants without third-shift operation, or during scheduled maintenance windows — running the system in low-load mode rather than shutting it down completely is the smarter choice for both equipment longevity and energy use. In this mode, airflow is reduced to 50–60% of nominal, the RH target is relaxed to 35–38%, and rotor regeneration temperature drops to 110°C. This strategy cuts energy consumption markedly and speeds up the return to setpoint when production resumes; PLC-based systems make these modes programmable.
VFD-Driven Airflow Control
Constant-speed fan motors waste energy during partial-load hours. A Variable Frequency Drive (VFD) that modulates fan output to actual moisture load brings substantial savings: because fan power scales with the cube of airflow (the Affinity Law), a 20% airflow reduction yields roughly a 49% reduction in fan power. In plants with variable conditioning-room occupancy this can lower annual energy spend markedly.
NKT – Nem Kontrol Teknolojileri
NKT – Nem Kontrol Teknolojileri is the authorised distributor in Türkiye for the Italian manufacturer TFT (Tecnofrigo Tuscany Srl). For jelly conditioning rooms it supplies ADP series silica-gel rotor dehumidifiers, supports unit selection using room conditions, target dew point and moisture load, and provides technical service and spare parts.
Design of the air-handling scheme and ductwork, installation, automation, commissioning and performance verification remain within the scope of the facility's designer and contractor.
References
- ASHRAE Handbook — Refrigeration, Chapter 42: Chocolates, Candies, Nuts, Dried Fruits, and Dried Vegetables, 2022.
- Hartel, R.W.; von Elbe, J.H.; Hofberger, R. — Confectionery Science and Technology, Springer, 2018.
- Edwards, W.P. — The Science of Sugar Confectionery, RSC Publishing, 2000.
- DIN EN 1507: Ventilation for Buildings — Sheet Metal Air Ducts.
- SMACNA: HVAC Air Duct Leakage Test Manual, 2nd Edition.
- Beckett, S.T. (ed.) — Industrial Chocolate Manufacture and Use, Wiley-Blackwell, 5th ed., 2017.
- TFT — Tecnofrigo Tuscany Srl, ADP Series Technical Data Sheets.