Evaporative (adiabatic) humidification adds moisture by contacting water directly with the airstream and evaporating it without first heating the water to its boiling point. Unlike steam systems, the bulk of electrical energy is not spent boiling water but instead on a high-pressure pump or a low-pressure pump + wetted-media loop. The heat of evaporation (≈ 0.68 kWh/kg) is taken from the air rather than from electricity; the unit's electricity is only for the pump and fan. The same process cools the air through the adiabatic evaporative cooling effect: in summer this is a cooling gain, while in winter the same energy is returned by reheat if the indoor temperature is held constant. This guide reads the evaporative energy balance from thermodynamic first principles all the way to HVAC-level balance, pump and fan energy, hygiene acceptability and a numerical comparison.
What Is Evaporative Humidification?
Evaporative humidification raises relative humidity and absolute humidity by evaporating water into the air directly, without first boiling it. The process is thermodynamically adiabatic: the latent heat required for evaporation is drawn from the air itself, the air cools, and water moves into the vapour phase. Steam (isothermal) systems use electrical energy to drive water to 100 °C and supply the latent heat externally; evaporative systems take that same latent heat from the sensible heat already present in the air, and that is the root of the energy gap.
Evaporative humidification is built on four core architectures. High-pressure atomisation (misting) pushes water through nozzles at 70 bar to produce <20 µm droplets; as droplet size shrinks, evaporation surface multiplies. Low-pressure spray + wetted media (evaporative cooler) circulates water across a ceramic or synthetic media at low pressure for natural evaporation over a large surface. Ultrasonic atomisation uses piezoelectric vibration to produce 1-5 µm mist, suiting smaller volumes and tight RH bands. Pad-type in-duct evaporative humidifier is the AHU-integrated form of the low-pressure design.
Figure 1. Steam vs Evaporative: Energy Flow Schematic
Where the Energy Comes From
In evaporative humidification, electricity use has three components. First, pump electricity: the 70 bar positive-displacement pump in high-pressure atomisation, or the circulation pump in wetted-media systems; power depends on the model and is taken from the product documentation. Second, water-treatment electricity: the booster pump for RO water. Third, the fan adder: in wetted-media systems the media's air-side resistance adds load to the AHU fan. Together these are small compared with the electricity a steam system uses to make steam; the main energy item, the heat of evaporation, comes from the air.
Compared with steam systems, the key difference is where the phase-change energy comes from. In a steam system, heating 1 kg of water from 20 °C to 100 °C takes ≈ 4.186 × 80 ≈ 335 kJ, and vaporising it at 100 °C ≈ 2,257 kJ; in total ≈ 2,592 kJ ≈ 0.72 kWh. The practical figure for electric steam humidifiers is ≈ 0.75 kWh/kg. In an evaporative system the heat of evaporation (≈ 2,450 kJ/kg ≈ 0.68 kWh/kg at around 20 °C) is not supplied from outside but drawn from the air's sensible heat; the unit's electricity is only for atomising or pumping water to the media. The comparison should therefore be made through the summer-winter energy balance, not a "times less" ratio.
Energy Difference vs Steam
The energy gap between steam and evaporative cannot be reduced to a single number, climate, run-hours, airflow and capacity all amplify it. The table summarises typical electrical consumption at common industrial capacities.
| System | Electricity | Source of the heat of evaporation | Heat for 100 kg/h |
|---|---|---|---|
| Steam, electrode / resistive | ≈ 0.75 kWh/kg (steam generation) | Electricity | ≈ 75 kW electricity |
| Steam, gas-fired (SKG4) | Auxiliary (fan, controls) | Natural gas | ≈ 72 kW heat + combustion losses |
| Evaporative high-pressure (SKH) | Pump only (product documentation) | Air | ≈ 68 kW from the air |
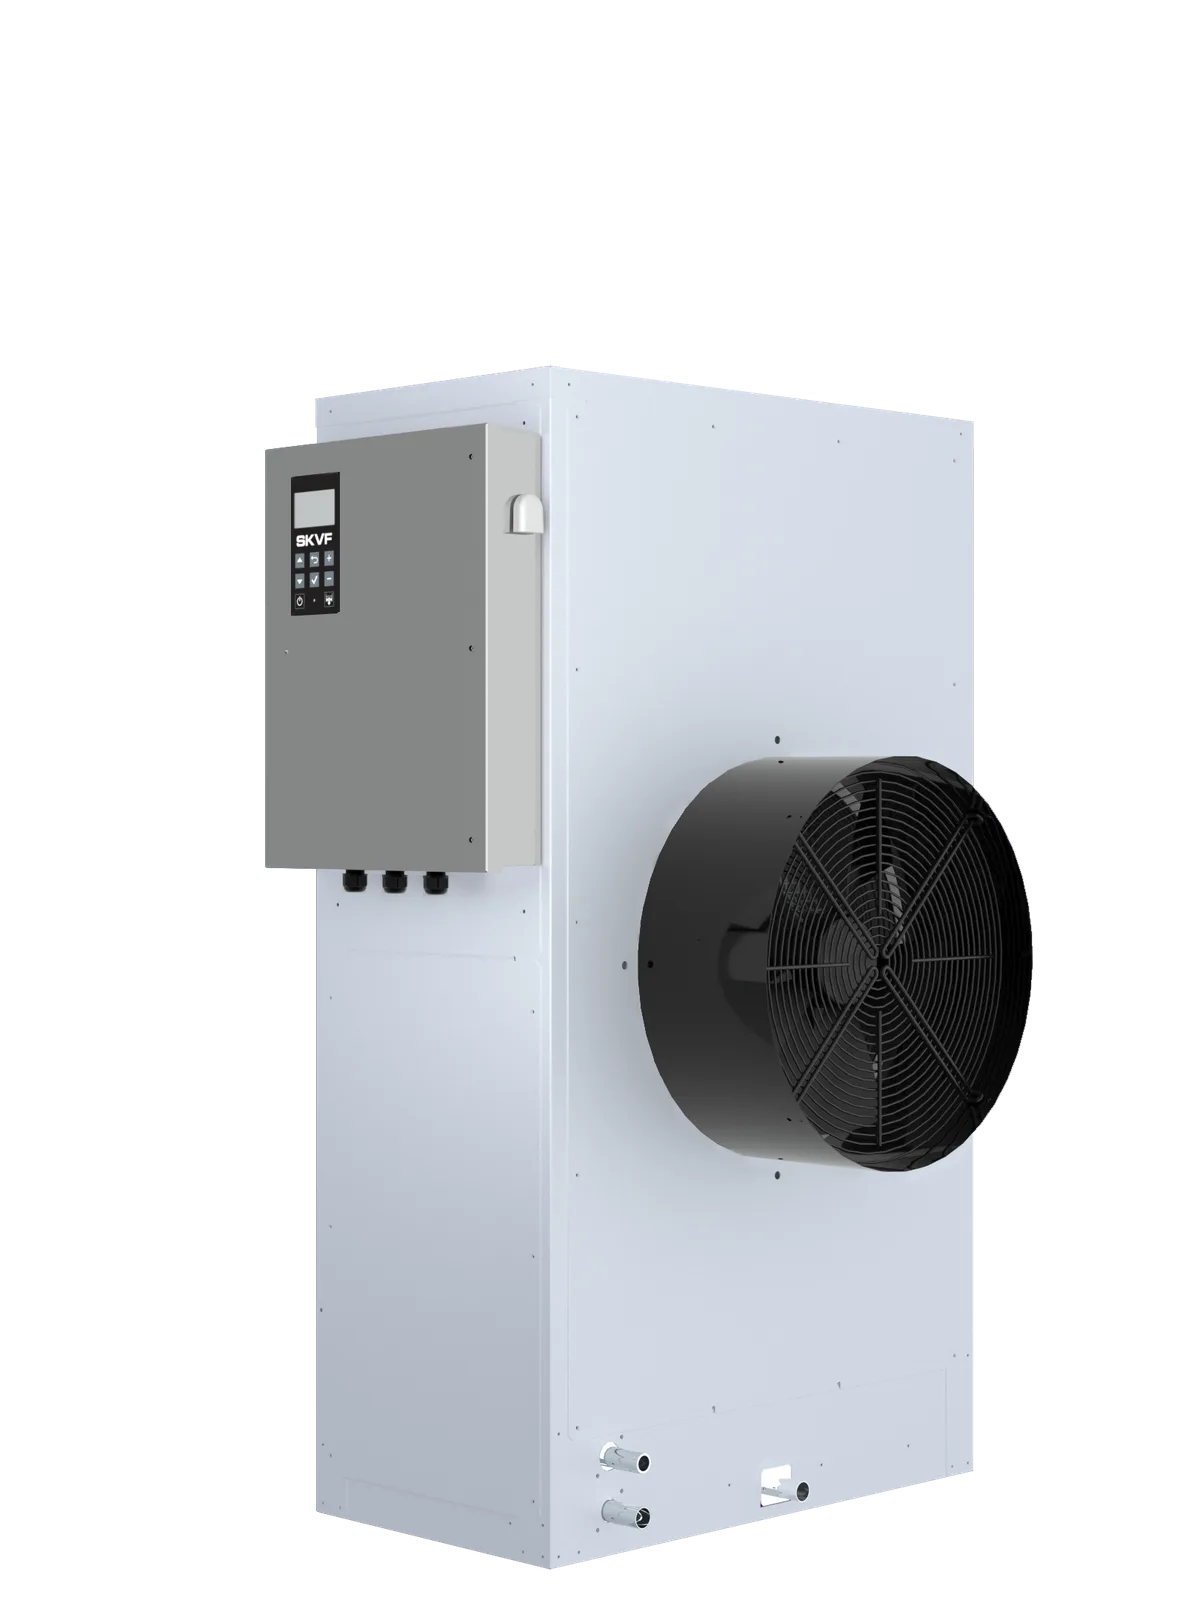
| Evaporative wetted media (SKV / SKVF) | Pump/fan only (SKVF < 1.5 kW) | Air | ≈ 68 kW from the air |
| Ultrasonic | Transducer electricity | Air | ≈ 68 kW from the air |
The table shows why the comparison cannot be expressed as a "times less" ratio: in a steam system the energy comes from electricity (or gas); in an evaporative system it comes from the air and, in winter, is returned by the heating system if the indoor temperature is held constant. The evaporative advantage is that this energy is supplied by a cheaper heat source than electricity (boiler, waste heat, heat pump) or, in summer, directly by the air. In high-capacity, summer-weighted facilities the difference is decisive; actual savings must be calculated from the facility's energy prices and operating profile.
Evaporative Cooling Effect
The second line item in the evaporative energy equation is the adiabatic cooling side benefit. Because the ≈ 2,450 kJ of latent heat required to evaporate 1 kg of water is taken from the air, the same process both adds moisture and cools the airstream. The amount of cooling depends on airflow and on the absolute-humidity addition; a quick estimate is ΔT (°C) ≈ Δw (g/kg) × 2.5. Air can cool at most to its wet-bulb temperature; in practice the calculation is done on a psychrometric chart. In hot, dry air the cooling can reach up to 12 K according to Neptronic data (e.g. 35 °C / 20% RH air has a wet-bulb temperature of ≈ 18.9 °C).
This side benefit reduces the cooling load directly. For a representative weaving floor with 30,000 m³/h airflow, a 6 °C summer adiabatic cooling step is equivalent to ≈ 60 kW of chiller capacity, i.e., 60 kW removed from chiller sizing. That cuts both capex and opex. A quick estimate: 60 kW × 2,000 h/year ÷ COP 3.5 → ≈ 34 MWh/year saved on cooling electricity.
Figure 2. Summer Adiabatic Cooling: Psychrometric Cycle
The psychrometric pattern shows the evaporative system effectively acting as a high-COP direct evaporative cooling unit on top of its humidification duty. For textile, food processing, greenhouse, print and data-centre pre-cooling, that single property is by itself a design rationale.
HVAC Energy Balance
A facility's true energy balance is read at the HVAC level, not the device level. Four line items move together: heating (winter), cooling (summer), humidification (winter + shoulder seasons) and outdoor-air conditioning (year-round). Evaporative humidification affects two of them: its own demand (humidification) is low and its side benefit (cooling) is high. Steam does the opposite: its own demand is high, it adds nothing to summer cooling and (equally) adds no unwanted heat to winter heating but provides no summer cooling assist either.
Seasonally the balance shifts. In winter the system focuses on humidification; pulling heat from the air is unwanted because we are already heating. So in winter steam runs "cleaner" by design, the energy supplied turns into moisture without affecting temperature. Evaporative in winter adds a cooling load that the heating coil must compensate for. On a purely winter design profile, evaporative's energy advantage largely disappears; the outcome depends on the source and price of the reheat. In summer the balance flips: extra cooling is valuable and evaporative's side benefit reduces chiller load directly.
In shoulder seasons (spring-autumn) and at sites with free-cooling / economiser cycles, evaporative pulls clearly ahead. In free-cooling mode the AHU draws 100% outdoor air; dry-but-cool outdoor air absorbs moisture and the system delivers both cooling and humidification in one step. This mode can run 1,500-3,000 h/year and forms a large line item in the annual balance at most sites.
Pump, Fan and Water Treatment Energy
Evaporative consumption is not just the device nameplate; three adders feed the real total. Pump energy is the backbone: high-pressure atomisation (SKH family) uses a 70 bar positive-displacement pump, and wetted-media systems (SKV/SKVF) a circulation pump; pump power depends on the model and is taken from the product documentation. Pump efficiency determines the device's overall energy figure; an IE3/IE4-class pump lowers annual consumption.
Fan adder comes from airflow resistance. Wetted media adds 30-80 Pa of pressure drop and increases AHU fan demand by 5-15%. High-pressure atomisation places a nozzle array in the duct with 10-30 Pa drop and a 2-5% fan adder. Ultrasonic systems offer essentially no airflow obstruction and therefore no fan adder, a real advantage in retrofits where the duct cannot be modified.
Water-treatment energy is nearly mandatory in evaporative systems. Hygienic atomisation and media systems run on RO feed; an RO unit consumes 1-3 kWh/m³. A 100 kg/h atomisation system running 3,000 h/year processes ≈ 300 m³ of RO water; RO electricity is a small item in the total budget. The RO reject stream sits at 30-40% of the input and adds to drainage load. This burden depends on the mineral content of the feedwater and is assessed from the facility's water analysis.
Hygiene Matters Too
The energy equation must not be read without acknowledging one of the evaporative system's structural limits, the hygiene perspective. Because water enters the air as a liquid droplet, Legionella and bacterial risk become engineering items that must be managed in design; in a steam system this risk is removed structurally because water is already at 100 °C. That difference defines where the energy-saving argument does and does not dominate.
A practical decision matrix: rooms with low-to-medium hygiene class (textile, print, greenhouse, food processing general floor, data-centre cooling) suit evaporative and energy saving is usually the primary driver. Rooms with high hygiene class (operating theatres, pharma cleanrooms, museum collection spaces, hospital sensitive rooms) should go to steam; here the energy gap sits below the hygiene assurance. Intermediate rooms (food packaging halls, precision electronics manufacturing, precision print rooms) can take a hybrid, evaporative for the bulk load + steam for tight-band finishing.
The engineering management of hygiene constraints (RO + UV + filtration + drainage + biofilm control) is the topic of a separate guide and covered in detail elsewhere in the adiabatic hygiene series. The take-away here: evaporative's energy advantage is structural and large, but it is meaningful only in the right application profile.
When Steam Is More Appropriate
In the following application profiles, steam is the structurally correct choice despite the energy gap:
- Hospital operating theatres and hygienic corridors: mineral-free steam with no microbiological risk is preferred in hygiene-critical areas; standards do not prescribe a specific technology.
- cGMP pharma cleanrooms: a tight RH band per product specification and a preference for mineral-free steam; evaporative systems are generally not preferred in these conditions.
- Museum collection spaces: a tight RH band set for the collection and a limited daily change are required; resistive steam + RO feed meets that.
- Sensitive electronics manufacturing (cleanroom Class 7-8): tight-band control + particulate-free air.
- Winter-dominant climate profile: sites whose annual run-hours are mostly winter benefit more from steam's isothermal winter advantage than from evaporative's summer cooling side benefit.
- Low capacity (< 50 kg/h): high-pressure atomisation is generally not economical at very small capacities; resistive steam or direct steam injection takes over.
When Evaporative Is More Appropriate
In the following profiles evaporative dominates on both energy balance and side benefit:
- Textile weaving and spinning floors (500-1,500 kg/h): high capacity + high RH target (65-80%) + the need to reduce summer chiller load. SKH high-pressure atomisation is the primary pick.
- Greenhouses and vertical farms: large volume + summer cooling demand + 80%+ RH target; the SKVF wetted-media system is the economical lead.
- Print and packaging halls: ±5% RH is enough, capacity is medium-high (200-800 kg/h), energy saving is meaningful.
- Food processing general floors (excluding cheese maturation) for main production: medium hygiene class; RO + UV + drainage combinations make evaporative viable.
- Data-centre free-cooling / pre-cooling: 2,000-3,000 h/year of adiabatic chiller operation delivers a high effective COP.
- Economiser cycle in AHUs: in shoulder seasons, 100% outdoor-air mode combines evaporative cooling and humidification in a single step.
- Industrial floor pre-cooling: 5-10 °C summer pre-cool reduces chiller load.
Simple Energy Comparison Example
Take a typical 300 kg/h textile weaving floor and compare annual energy. Representative site profile: RH target 75%, annual run-hours 3,500 (winter 2,000 h, summer 1,500 h).
| Line item | Steam (resistive) | Evaporative (SKH high-pressure) |
|---|---|---|
| Winter (2,000 h): humidification energy | 300 × 0.75 ≈ 225 kW electricity → ≈ 450 MWh electricity | 300 × 0.68 ≈ 204 kW from the air → ≈ 408 MWh reheat (boiler / heat pump) |
| Summer (1,500 h): humidification energy | ≈ 225 kW electricity → ≈ 338 MWh electricity | ≈ 204 kW cooling gain (≈ 306 MWh of cooling) |
| Unit electricity | Steam generation (above) | Pump + RO only (from product documentation; e.g. 3 × SKH-100) |
| Outcome | All energy from electricity | Energy from the heating system in winter, from the air in summer |
This example uses a single capacity and climate profile; real projects price the site's hourly load profile, capacity distribution, water quality and maintenance lines into the analysis. The cost difference depends on which source (natural gas, waste heat, heat pump) covers winter reheat and at what price, and on the value of the summer cooling gain; it must therefore be calculated from the facility's energy prices.
NKT Approach
NKT – Nem Kontrol Teknolojileri covers the wide capacity-application matrix with three Neptronic evaporative product lines (SKVF, SKH, SKV) and the SKD direct steam injection line. SKVF, the evaporative cooler, is the energy-saving backbone with its low-pressure wetted-media architecture; it is the primary pick for textile, greenhouse, industrial-floor pre-cooling and free-cooling applications. SKH, high-pressure atomisation, is the main product with <20 µm droplets (70 bar; 20, 50 and 100 kg/h models), for applications where homogeneous in-duct distribution and large-volume applicability matter; designed for textile weaving, print, packaging and large industrial sites.
SKV, the evaporative humidifier, is a wetted-media solution installed inside the air-handling unit and sized for each project. SKD is not evaporative but a steam system that injects facility boiler steam directly into the air; it is an economical alternative where boiler steam exists but is not preferred in hygiene-critical areas.
As NKT – Nem Kontrol Teknolojileri, we are the authorised Turkish distributor of Neptronic humidifiers; we provide equipment supply, technical support in equipment selection, technical service and spare parts. Engineering design, installation and commissioning are within the scope of the facility's design engineer and installer. Four inputs are assessed together when selecting an evaporative system: (1) the facility's annual load profile and seasonal distribution, (2) hygiene class and RH tolerance band, (3) water analysis and water treatment need, (4) the summer cooling gain and winter reheat within the HVAC system.
Evaporative humidification is a technology family that uses electricity only for the pump and fan, takes the heat of evaporation from the air and delivers adiabatic cooling as a by-product. The "steam vs evaporative" answer is not a single number; it is an engineering decision shaped by climate profile, capacity, hygiene class and seasonal load distribution. Textile weaving, greenhouses, print, large industrial floors and data-centre pre-cooling favour evaporative clearly; hospital, pharma cleanroom, museum and sensitive-electronics manufacturing favour steam structurally.
The right choice answers three questions together: (1) What is the site's annual humidification load and seasonal distribution? (2) Does the application's hygiene class and RH tolerance band suit evaporative? (3) How much does the adiabatic side-cooling reduce summer chiller load? These questions should be answered by psychrometric analysis and the facility's energy data; the technology selection comes out of the engineering analysis, not the nameplate.